




Toolox® Machining
Machining recommendations for Toolox®
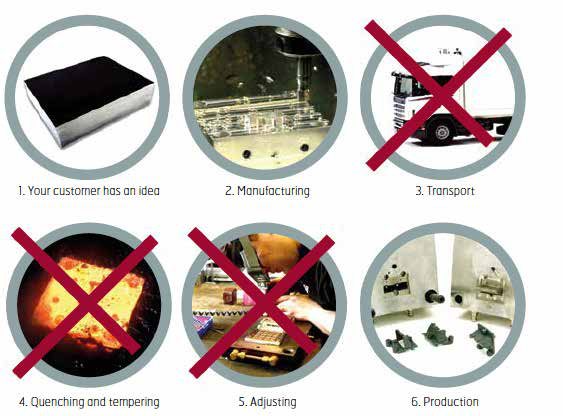
Toolox® is a modern quenched and tempered prehardened engineering and tool steel, delivered with measured and guaranteed mechanical properties. The basic idea is to save you time by delivering Toolox® heat treated and ready to use. It provides you with lower costs, reduced risks and saves you valuable time in your production process due to its excellent machinability.
Toolox® is based on the same low carbon content as in Hardox® and Strenx®, but it is specially developed for tools and machine components working at high temperatures. It has excellent fatigue properties, and you can increase the surface hardness with nitriding or PVD coatings to gain more control over the service life of your tools or components.
Shorter lead time from concept to production
In the information that follows, you will find our recommendations of tools to process Toolox®. Similar tools from other suppliers might work, but here are the ones we have tested so far.
All content in this brochure should be considered as recommendations. Machining contains many different parameters that can and will affect the end result. Optimization of cutting data should always take place at the machine to be used for manufacturing.
Drilling recommendations
It is recommended to use drills with an internal coolant supply when drilling Toolox®. Internal coolant:
- Is always to be preferred to avoid chip jamming.
- Should always be used at hole depth above 3 times the drill diameter.
- Never use a HSS drill with external cooling in a horizontal drilling machine.
- Coolant mix 8 – 12%.
To make a hole with a tight tolerance, a good surface finish and a long service life of the drill, the following is required:
- Make sure that the runout on the drill is as small as possible. For solid carbide drills, the runout should not exceed 0,02 mm.
- Use the shortest possible drill for maximum stability.
- Chip breaking and chip evacuation must always be good.
- Coolant supply and pressure need to be satisfactory.
- A collet and tool shank in bad condition will ruin an otherwise perfect setup.
- The machine should be in good condition.
- A good clamping of the workpiece is necessary.
Formulas and definitions, drilling
- Vc = Dc × π × n / 1000
- n = Vc × 1000 / (π × Dc)
- Vf = fn × n
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- fn = feed per revolution (mm/r)
- Vf = penetration rate (mm/min)
- Dc = drill diameter (mm)
Solid cemented carbide drill
First choice for smaller diameter and when closer diameter tolerance is required. Works well for short or relatively deep holes. The drill is sensitive to vibrations and should be used together with high precision chucks.
Solid cemented carbide drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn), mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 3,0 – 5,0 mm — Min - Max | Ø 3,0 – 5,0 mm — Start value | Ø 5,01 – 10,0 mm — Min - Max | Ø 5,01 – 10,0 mm — Start value | Ø 10,01 – 15,0 mm — Min - Max | Ø 10,01 – 15,0 mm — Start value | Ø 15,01 – 20,0 mm — Min - Max | Ø 15,01 – 20,0 mm — Start value |
|---|---|---|---|---|---|---|---|---|---|
Toolox® 33 | 65 – 90 | 0,08 – 0,15 | 0,10 | 0,09 – 0,16 | 0,12 | 0,16 – 0,22 | 0,18 | 0,22 – 0,28 | 0,25 |
Toolox® 40 | 50 – 65 | 0,06 – 0,12 | 0,08 | 0,08 – 0,15 | 0,11 | 0,16 – 0,20 | 0,16 | 0,16 – 0,24 | 0,20 |
Toolox® 44 | 40 – 60 | 0,06 – 0,11 | 0,07 | 0,08 – 0,13 | 0,10 | 0,12 – 0,18 | 0,15 | 0,16 – 0,20 | 0,18 |
Long hole drilling with 16 – 20 × Dc
Clamping of this type of drill should be done with high precision chucks. Possible hole tolerance H8-H9. Cutting fluid pressure > 20 bar.
Drilling strategy for drills > 12 × Dc:
- Pre-drill a hole 1,5-2 × Dc. Use a solid cemented carbide drill with the same diameter; it is recommended to use a shallow point angle, 150°.
- When entering with the long drill, start the machine spindle at a low speed not higher than 500 rpm, with no cooling.
- Insert the drill into the hole, stopping about 1 mm above the bottom of the pre-drilled hole.
- At full drilling depth, reduce the speed to 500 rpm and turn off the cutting fluid.
- Retract the drill by 4 times the machine feed to avoid re-scratching the surface of the hole.
Long hole drilling, 16 – 20 × Dc. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn), mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 6,0 mm — Min - Max | Ø 6,0 mm — Start value | Ø 8,0 mm — Min - Max | Ø 8,0 mm — Start value | Ø 10,0 mm — Min - Max | Ø 10,0 mm — Start value | Ø 12,0 mm — Min - Max | Ø 12,0 mm — Start value |
|---|---|---|---|---|---|---|---|---|---|
Toolox® 33 | 50 – 70 | 0,06 – 0,12 | 0,14 | 0,14 – 0,20 | 0,16 | 0,17 – 0,24 | 0,19 | 0,18 – 0,26 | 0,20 |
Toolox® 40 | 50 – 65 | 0,10 – 0,15 | 0,12 | 0,11 – 0,18 | 0,14 | 0,13 – 0,22 | 0,16 | 0,15 – 0,24 | 0,18 |
Toolox® 44 | 40 – 60 | 0,08 – 0,14 | 0,11 | 0,10 – 0,18 | 0,13 | 0,12 – 0,21 | 0,15 | 0,14 – 0,23 | 0,17 |
Exchangeable tip drills
A good first choice when drilling medium-sized holes. The exchangeable tip provides for an economical solution.
- The drill has close hole tolerance.
- The steel-made drill body provides the drill with toughness.
- Used for short or relatively deep holes.
Exchangeable tip drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn), mm/rev / Min - Max.
Steel grade | Cutting speed (Vc), m/min | Ø 7,5 – 12,0 mm | Ø 12,01 – 20,0 mm | Ø 20,01 – 25,0 mm | Ø 25,01 – 30,0 mm |
|---|---|---|---|---|---|
Toolox® 33 | 50 – 80 | 0,10 – 0,16 | 0,15 – 0,23 | 0,18 – 0,27 | 0,20 – 0,30 |
Toolox® 40 | 50 – 65 | 0,08 – 0,15 | 0,12 – 0,22 | 0,15 – 0,25 | 0,17 – 0,27 |
Toolox® 44 | 40 – 60 | 0,08 – 0,14 | 0,12 – 0,20 | 0,14 – 0,22 | 0,16 – 0,25 |
Indexable insert drill
This drill produces holes at a low cost, due to the fact that it is possible to use several sides on the inserts. This drill has no tip that centers the drill, therefore use as short drills as possible to achieve good lateral stability when used in Toolox®.
- Medium and large diameter holes.
- Medium tolerance demands.
- A drill suitable for boring operations.
The recommendations apply to a drill with a max drilling depth of 2 × Dc.
Indexable insert drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn), mm/rev / Min - Max.
Steel grade | Cutting speed (Vc), m/min | Ø 12,0 – 20,0 mm | Ø 20,01 – 30,0 mm | Ø 30,01 – 40,0 mm | Ø 40,01 – 60,0 mm |
|---|---|---|---|---|---|
Toolox® 33 | 80 – 140 | 0,04 – 0,12 | 0,06 – 0,16 | 0,08 – 0,20 | 0,10 – 0,21 |
Toolox® 40 | 70 – 130 | 0,04 – 0,12 | 0,06 – 0,16 | 0,08 – 0,20 | 0,10 – 0,21 |
Toolox® 44 | 60 – 110 | 0,04 – 0,12 | 0,06 – 0,16 | 0,08 – 0,20 | 0,10 – 0,21 |
HSS drills
Use HSS drills only when you have unstable machine conditions. If the machine conditions are good you can use a different solid cemented carbide drill or a drill with exchangeable tip.
Use an HSS-Co drill (8% Co) with a small helix angle and a robust core that can withstand high torques. Individual holes can be drilled with an ordinary HSS drill.
HSS-Co drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn), mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 5 mm | Ø 10 mm | Ø 15 mm | Ø 20 mm | Ø 25 mm | Ø 30 mm |
|---|---|---|---|---|---|---|---|
Toolox® 33 | ≈ 15 | 0,10 | 0,10 | 0,16 | 0,23 | 0,30 | 0,35 |
Toolox® 40 | ≈ 9 | 0,05 | 0,10 | 0,16 | 0,22 | 0,28 | 0,35 |
Toolox® 44 | ≈ 7 | 0,05 | 0,09 | 0,15 | 0,20 | 0,25 | 0,30 |
Milling recommendations
Clamping
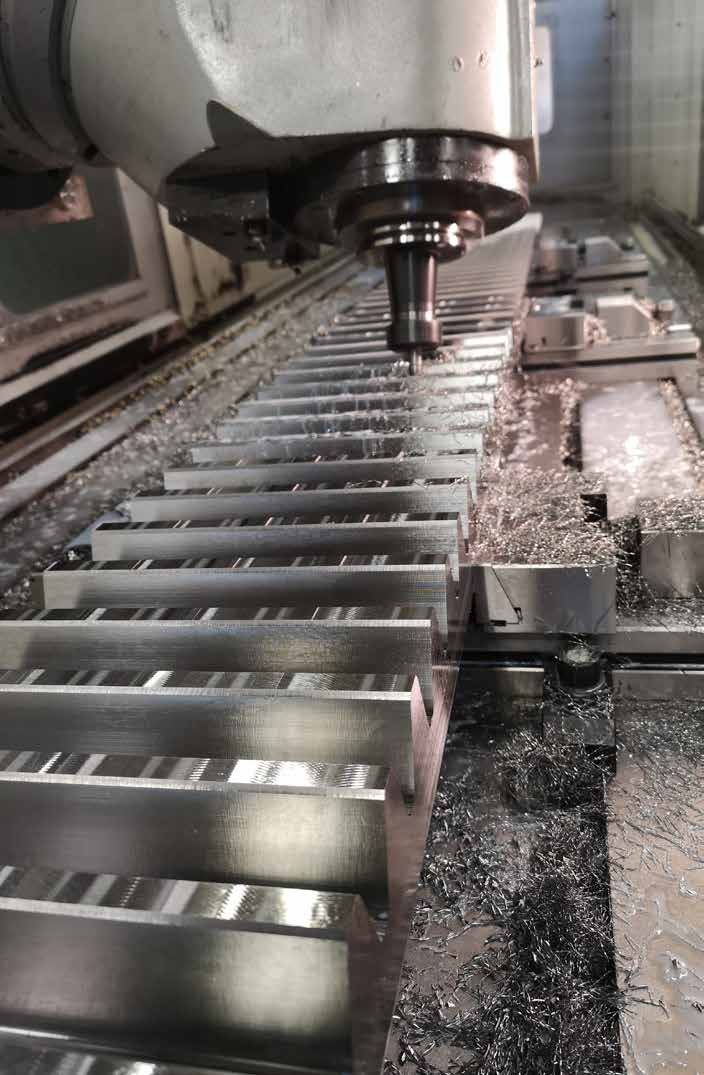
Toolox® has a very low level of residual stresses. To get the full effect make sure to use deformation-free clamping. If blanks are gas cut, mill off 5-10 mm from the gas-cut edge to get a blank free from residual stresses.
The machinability of Toolox® has been improved. During milling you will notice it because the chips produced are very bluish. We have modified the carbide morphology as compared to traditional tool steels, using less carbon in Toolox®. Therefore, the heat generated during milling is transferred into the chip and not into the cutting edge/workpiece.
Milling advice
- Position the cutter off-centre (to the left) to achieve a thicker chip at the entry and to avoid a thick chip on the exit.
- Avoid cutting through the center line of the cutter, because this can generate vibration.
- Always use down milling (climb milling).
- The recommendation is that the radial engagement of the cutter (ae) should be 25 or 75-80% of the diameter.
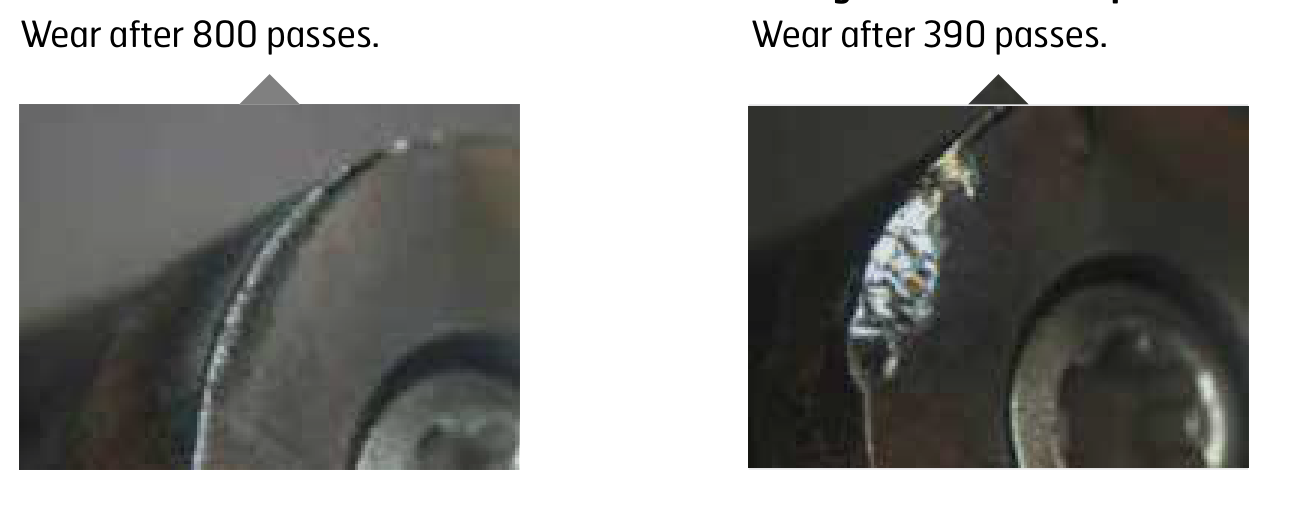
If you enter the workpiece with the roll-into-cut method, the chip thickness on the exit is always zero, and it will help to give a longer tool life. The programmed radius for roll-into-cut is Dc / 2 + 2.
Roll-into-cut. Wear after 800 passes with the roll-into-cut method, against wear after 390 passes going straight into the workpiece. Image: Sandvik Coromant AB.
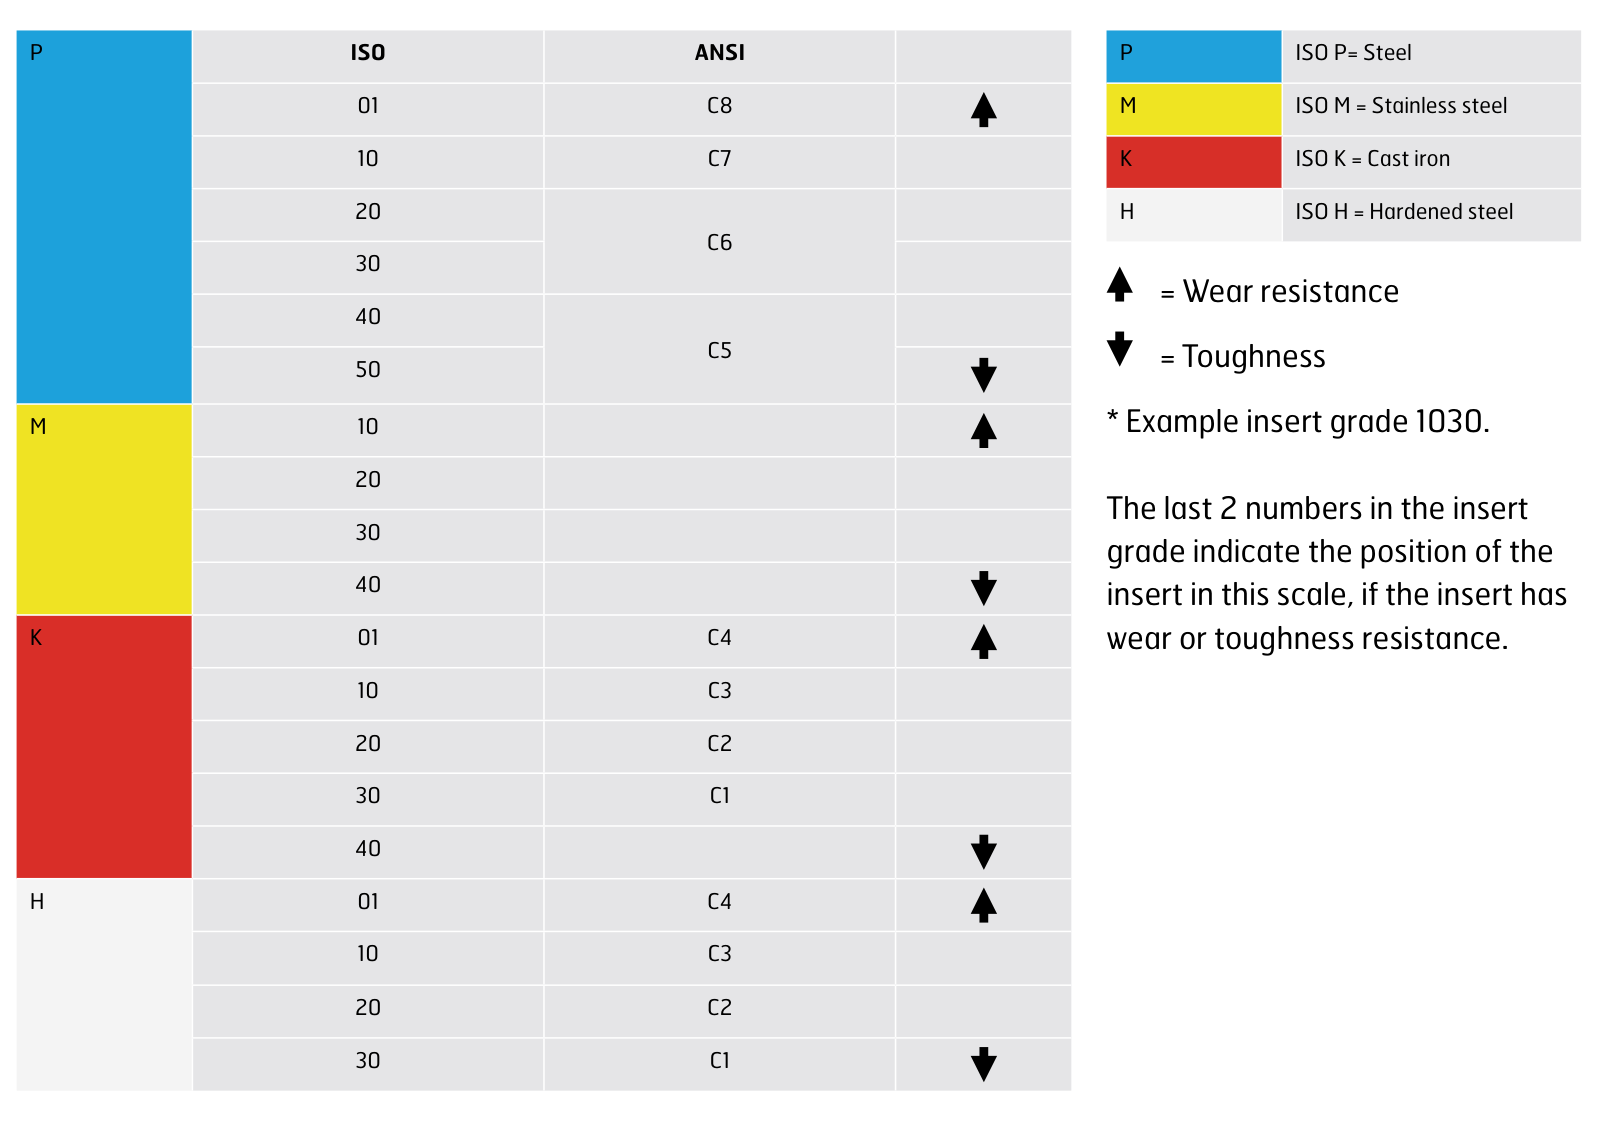
Insert grades for milling. ISO and ANSI grade codes against the P, M, K and H workpiece material classes, with the wear-resistance and toughness direction of the scale.
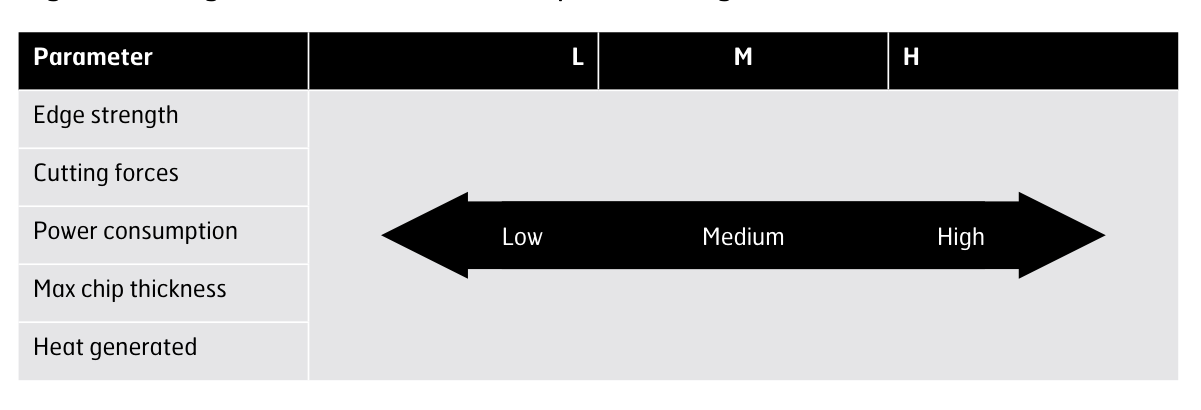
Insert geometry. Edge strength, cutting forces, power consumption, maximum chip thickness and heat generated across the L, M and H geometries.
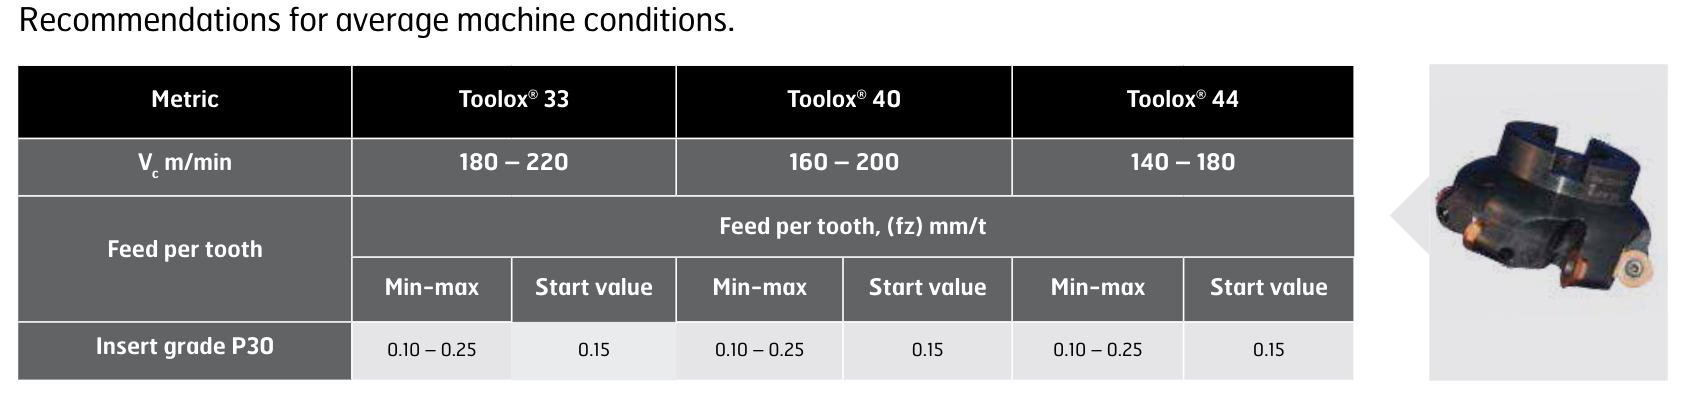
Face milling recommendations
Face milling, 45° entering angle. Recommendations for average machine conditions, insert grade P30.
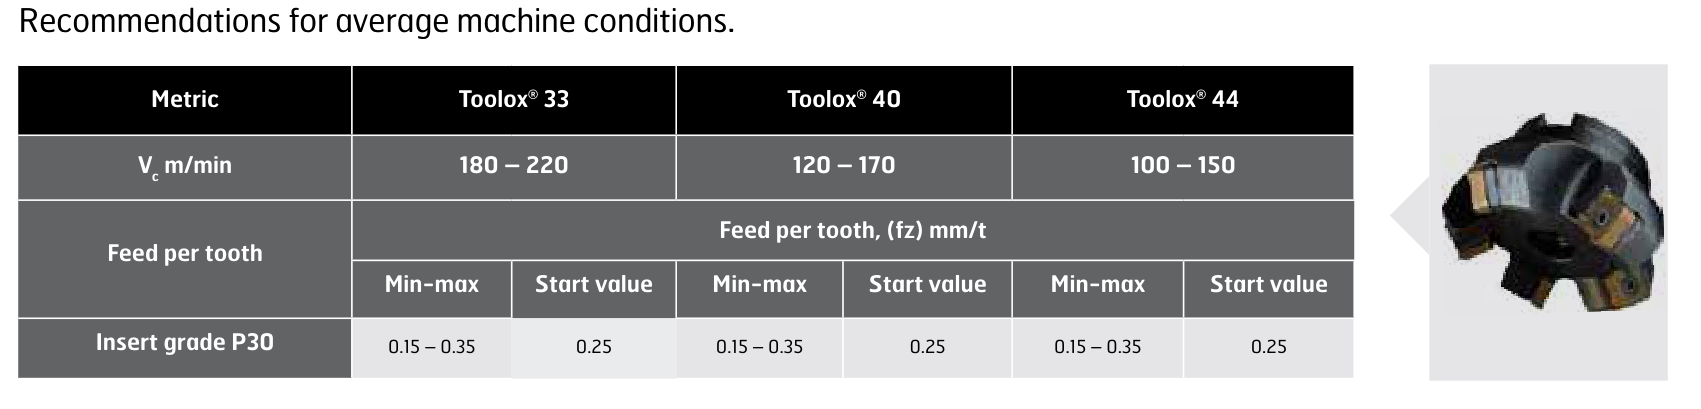
Face milling, round insert. Recommendations for average machine conditions.
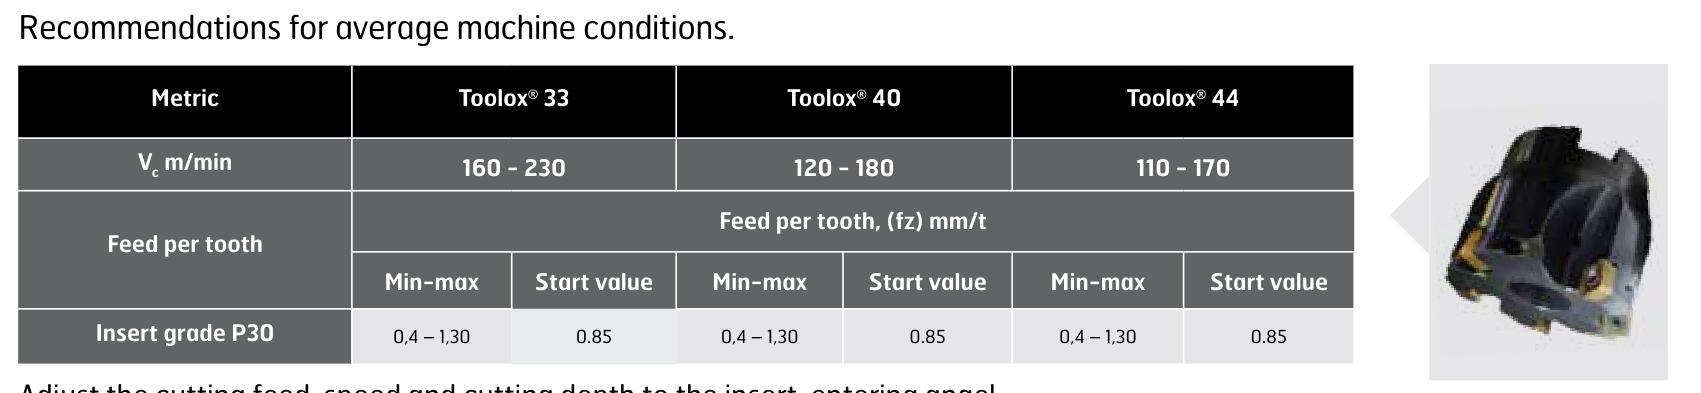
Shoulder / face milling. Recommendations for average machine conditions.
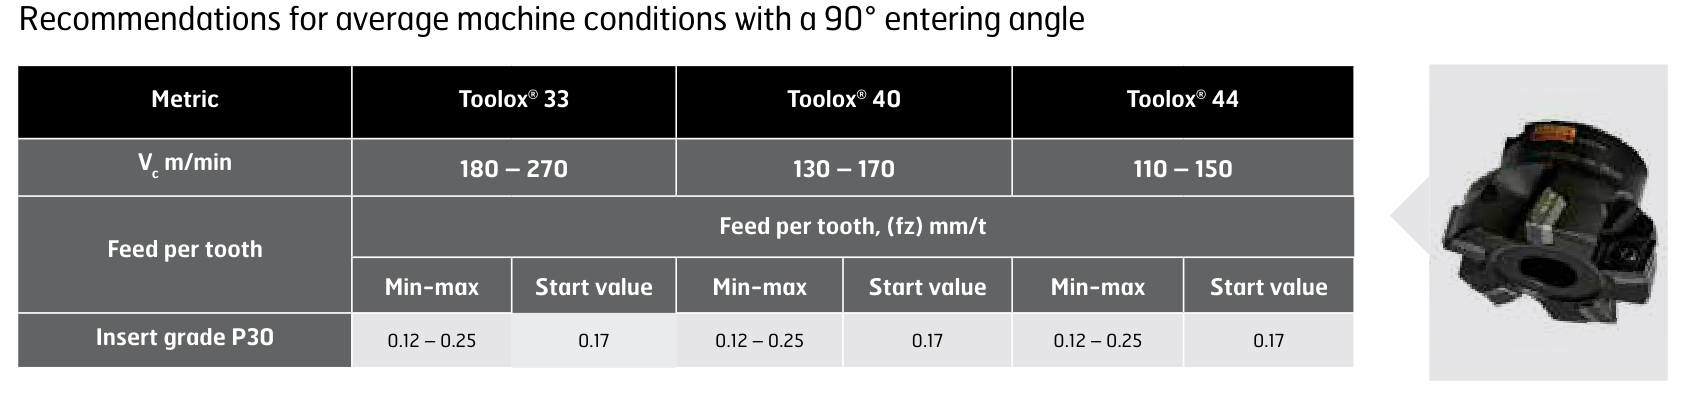
High feed face milling. Recommendations for average machine conditions.
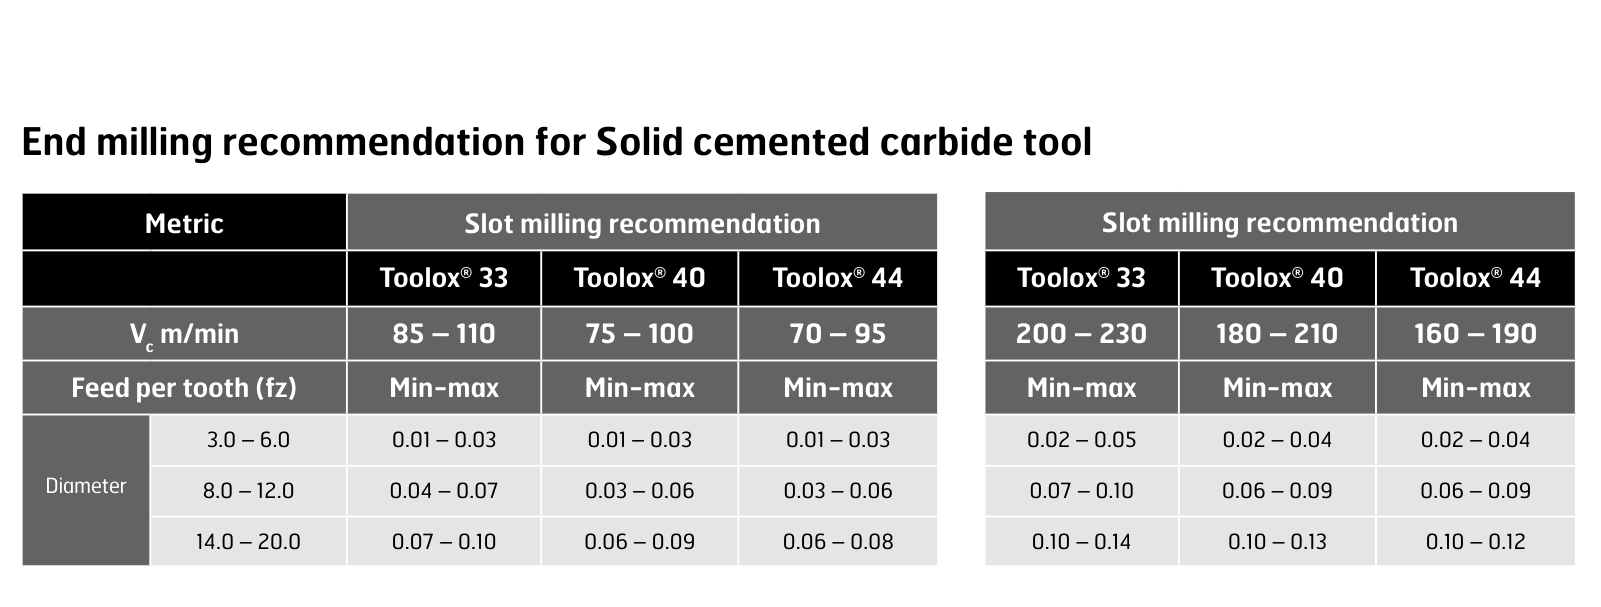
Slot milling and end milling. Recommendation for a solid cemented carbide tool, by cutter diameter.
Turning recommendations, Toolox® round bars
Formulas and definitions, turning
- Vc = Dm × π × n / 1000
- n = Vc × 1000 / (π × Dm)
- vf = n × fn
- π = 3,14
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- fn = feed per revolution (mm/r)
- vf = feed rate (mm/min)
- Dm = machined diameter (mm)
- ap = cutting depth (mm)
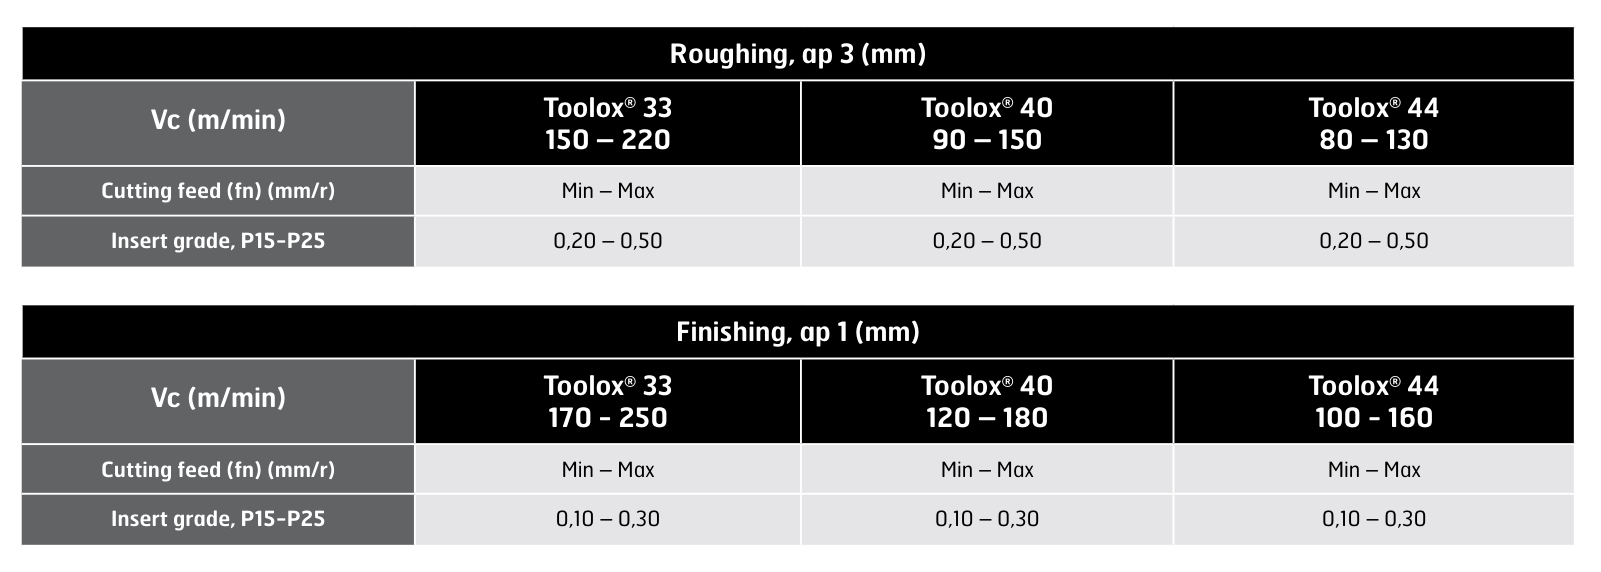
Turning, roughing and finishing. Roughing at ap 3 mm and finishing at ap 1 mm, insert grade P15-P25.
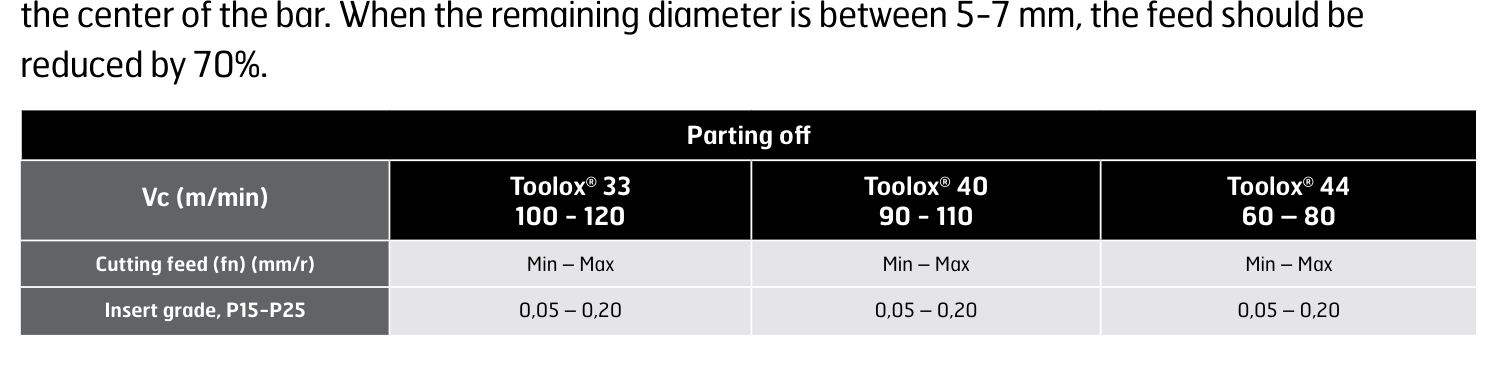
Parting off. Cutting data for parting off Toolox® round bars.
Threading recommendations
Cutting speeds for tapping are 7 – 10 m/min for Toolox® 33, 4 – 9 m/min for Toolox® 40 and 3 – 5 m/min for Toolox® 44. The spindle speeds that follow from those are listed by thread size below.
Tapping. Spindle speed in rpm by thread size. Cutting speed Vc is 7 – 10 m/min for Toolox® 33, 4 – 9 m/min for Toolox® 40 and 3 – 5 m/min for Toolox® 44.
Size | Toolox® 33 | Toolox® 40 | Toolox® 44 |
|---|---|---|---|
M5 | 445 – 635 | 255 – 570 | 190 – 320 |
M6 | 370 – 530 | 210 – 475 | 160 – 265 |
M8 | 270 – 400 | 160 – 360 | 120 – 200 |
M10 | 220 – 320 | 125 – 285 | 95 – 160 |
M12 | 185 – 265 | 105 – 240 | 80 – 130 |
M16 | 140 – 200 | 80 – 180 | 60 – 100 |
M20 | 110 – 160 | 60 – 140 | 45 – 80 |
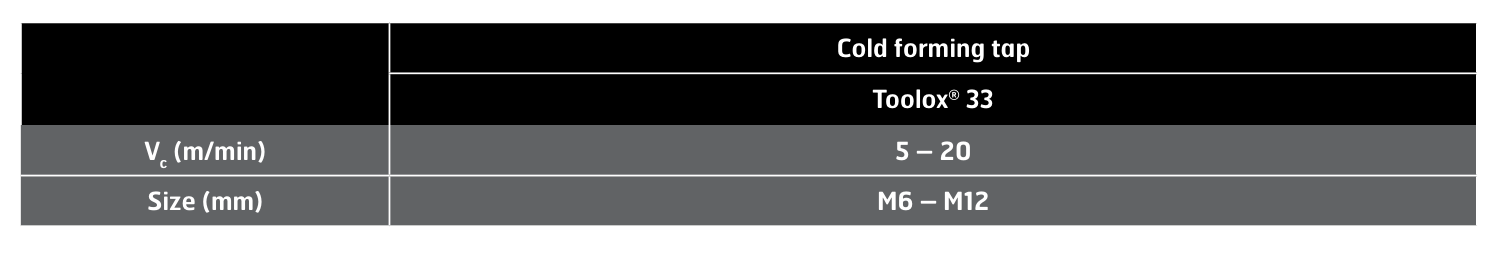
Cold forming tap. Cold forming tapping is recommended for Toolox® 33 only, at 5 – 20 m/min in sizes M6 – M12.
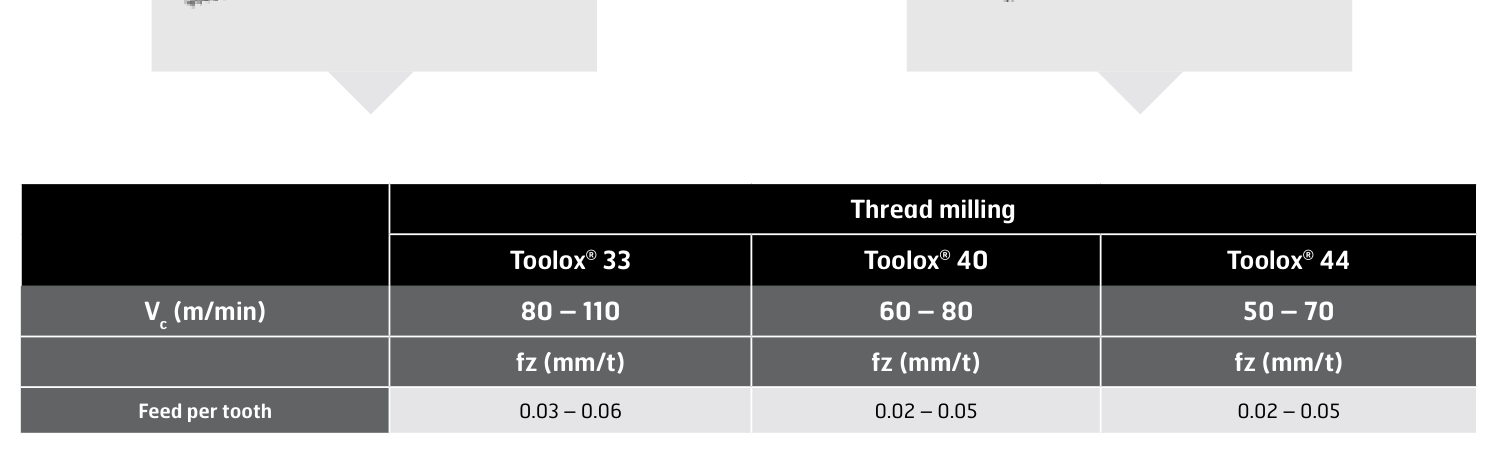
Thread milling. Cutting speed and feed per tooth by grade.
Recommendation counterboring and countersinking
Use a counterbore or countersink with indexable inserts. Feed per revolution is 0.10 – 0.20 mm/r for all three grades in both operations. The countersinking cutting speeds are 30% lower than the counterboring ones, in line with SSAB’s general rule for countersinking.
Counterboring. Spindle speed in rpm by counterbore diameter. Cutting speed Vc is 40 – 80 m/min for Toolox® 33, 25 – 70 m/min for Toolox® 40 and 20 – 50 m/min for Toolox® 44; feed per revolution 0.10 – 0.20 mm/r.
Dc | Toolox® 33 | Toolox® 40 | Toolox® 44 |
|---|---|---|---|
19 mm | 670 – 1340 | 420 – 1175 | 335 – 840 |
24 mm | 530 – 1060 | 330 – 930 | 265 – 665 |
34 mm | 375 – 750 | 235 – 655 | 185 – 470 |
42 mm | 300 – 600 | 190 – 530 | 150 – 380 |
57 mm | 225 – 440 | 140 – 390 | 110 – 280 |
Countersinking. Spindle speed in rpm by countersink diameter. Cutting speed Vc is 28 – 56 m/min for Toolox® 33, 18 – 49 m/min for Toolox® 40 and 14 – 35 m/min for Toolox® 44; feed per revolution 0.10 – 0.20 mm/r.
Dc | Toolox® 33 | Toolox® 40 | Toolox® 44 |
|---|---|---|---|
19 mm | 469 – 938 | 302 – 821 | 235 – 586 |
24 mm | 371 – 743 | 239 – 650 | 186 – 464 |
34 mm | 262 – 524 | 169 – 459 | 131 – 328 |
42 mm | 212 – 424 | 136 – 371 | 106 – 265 |
57 mm | 156 – 313 | 101 – 274 | 78 – 195 |
Tool recommendations for Toolox®
The tools below are grouped by type. Article numbers are reproduced exactly as SSAB prints them, including the wildcard characters that stand for the size-dependent part of the number. Similar tools from other suppliers might work; these are the ones SSAB has tested.
High speed steel drill. High speed steel drill alloyed with 8% cobalt (HSS-Co 8%). High speed steel drill standard. Only for Toolox® 33. High speed steel drill alloyed with cobalt (DRILL BIT COBALT”S”+X-ALCR DIN1897N HARDOX STUB). High speed steel drill alloyed with cobalt (DRILL BIT COBALT”S”+X-ALCR TAPER STUB).
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Alpen-MayKestag, Austria | HSS-E Co 8 Taper Shank Drills, WN 103 | 832xxxxx | https://www.maykestag.com/en/ |
Witec, Germany | TYPE WITEC MN | 2-135 15 VAP | http://witec-tools.de/index.php?content=produkte&lang=en |
Dormer Pramet | HSS A100 | A100xx.xx | https://www.dormerpramet.com/en-gb/pages/default.aspx?country=gb |
Izar, Spain | Ref 1054 | Article nr: 32xxx | https://www.izartool.com/ |
Izar, Spain | Ref 1154 | xxxxx | https://www.izartool.com/ |
Solid cemented carbide drill. Solid cemented carbide drill. Solid cemented carbide drill. Long hole drilling with 16 – 20xD.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
SECO TOOLS, Sweden | Seco Feedmax | SD203A-xx.xx-xx-xxxx-x | https://www.secotools.com/ |
Sandvik Coromant AB, Sweden | Corodrill® Delta-C | R840-xxxx-30-A1A | https://www.sandvik.coromant.com/ |
SECO TOOLS, Sweden | Seco Feedmax | SD216A-xx.xx-xx-xxxx-x | https://www.secotools.com/ |
Sandvik Coromant AB, Sweden | CoroDrill 861 | 861.1-xxxx-xxxxxx-xx | https://www.sandvik.coromant.com/ |
Indexable insert drill. Indexable insert drill.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Sandvik Coromant AB, Sweden | Corodrill 880 | 880-xxxxxxxx-xx | https://www.secotools.com/ |
Drill with exchangeable drill tip. Drill with exchangeable drill tip. Drill tip grade: IC908.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Iscar, Israel | Chamdrill | DCM xxx-xxx-xxA-xx | https://www.iscar.com/ |
Iscar, Israel | SumoCham | DCN xxx-xxx-xxA-xx | https://www.iscar.com/ |
Seco Tool AB, Sweden | Crownloc | SD103-xx.xx-xx-xxxx | https://www.secotools.com/ |
Taps. HSSE tap with TiCN coating. HSSE-PM tap with TiCN coating. HSSE-PM tap with TiN coating.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Emuge Franken, Germany | Rekord 1D-TI-TiCn, Rekord 2D-TI-TiCN | B0459601.xxxx, C0459601.xxxx | https://www.emuge-franken.se/en/ |
Manigley, Switzerland | 131/3 DUO | 433xx | http://manigley.ch/ |
Emuge Franken, Germany | Rekord 1C-TI-TiCn, Rekord 2C-TI-TiCN | B0309601.xxxx, C0309601.xxxx | https://www.emuge-franken.se/en/ |
Manigley, Switzerland | 105/4 DUO | 433xx | http://manigley.ch/ |
Emuge Franken, Germany | InnoForm2-Steel | C5267F00.xxxx | https://www.emuge-franken.se/en/ |
Thread milling cutters. Solid carbide thread milling cutter with TiCN coating. Solid carbide thread milling cutter with TiAlCN coating.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Emuge Franken, Germany | GSF-1,5xD-IKZ-HB-TiCN | GF333106xxxx | https://www.emuge-franken.se/en/ |
Smicut, Sweden | Solid Carbide Thread Mill | NBxxxxxCxxx.xISO AC | https://smicut.com/en/ |
Counterbore and countersink. Use counterbore with indexable inserts that always have a grade number ending in U. Use countersink with indexable inserts that always have a grade number ending in U.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Granlund Tool AB, Sweden | WHV Counterbore | xWHV-xx.x | http://www.granlund.com/ |
Granlund Tool AB, Sweden | KV Countersink | xKV9-xx.x | http://www.granlund.com/ |
End milling. Solid end milling cutter with Siron-A coating.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Seco Tool AB, Sweden | JS 554 Siron-A | JS 554 xxxx | https://www.secotools.com/ |
Milling with inserts. Face milling with Coromill 345. Face milling with Coromill 300. Shoulder/Face milling with Coromill 490. Face milling with Mill4Feed. Face milling with Coromill 210.
Supplier | Tool name | Article nr | Insert grade | Web |
|---|---|---|---|---|
Sandvik Coromant AB, Sweden | Coromill 345 | 345-xxxxxx-13x | 1030 | https://www.sandvik.coromant.com/ |
Sandvik Coromant AB, Sweden | Coromill 300 | R300-xxxxxx-xxx | 1030 | https://www.sandvik.coromant.com/ |
Sandvik Coromant AB, Sweden | Coromill 490 | 490-xxxxxx-xxx | 1030 | https://www.sandvik.coromant.com/ |
Iscar, Israel | Mill4Feed | FFQ4 xxxx-x-xxx-xx | IC808 | https://www.iscar.com/ |
Sandvik Coromant AB, Sweden | Coromill 210 | 210-xxxxxx-xxx | 1030 | https://www.sandvik.coromant.com/ |
Contact and more information
Contact your local SSAB representative or Tech Support at [email protected], or visit www.toolox.com.
All content in this brochure should be considered as recommendations. Optimization of cutting data should always take place at the machine to be used for manufacturing.