




Strenx® Machining
Machining recommendations for Strenx®
Strenx® performance steel can be machined with high speed steel (HSS) or cemented carbide (CC) tools. This brochure includes our suggestions for cutting data (feeds and speeds) and the selection of tools. Other factors that should be taken into account in machining operations are also discussed.
The proposals have been drawn up following our own tests on tools of various makes and in consultation with leading tool manufacturers.
The recommended cutting data and selection of tools also apply to our Strenx® MC, Plus and MC Plus of equal strength grade. For Strenx® 600 MC, Strenx® 650 MC, Strenx® 100, Strenx® 100 XF and Strenx® 110 XF use the same data as for Strenx® 700.
Typical properties for Strenx®
Hardness in Brinell (HBW) | Hardness in Rockwell (HRC) | Tensile strength, Rm (N/mm2) | |
|---|---|---|---|
Strenx® 700 | ~260 | ~24 | ~860 |
Strenx® 900 | ~300 | ~29 | ~935 |
Strenx® 960 | ~320 | ~32 | ~990 |
Strenx® 1100 | ~430 | ~43 | ~1340 |
Strenx® 1300 | ~500 | ~49 | ~1580 |
Tool suppliers we recommend and have collaborated with
All the recommendations in this brochure are based on results after practical testing of numerous tools in different situations. We collaborate with some of the world's leading tool manufacturers which we highly recommend using.
Tool suppliers we recommend and have collaborated with
Dorato Tools | www.d-tools.se |
|---|---|
Emuge Franken | www.emuge-franken.de |
Granlund Tools | www.granlund.com |
Hoffmann Group | www.hoffmann-group.com |
IZAR Cutting Tools | www.izartool.com |
ISCAR | www.iscar.com |
Komet Group | www.kometgroup.com |
Manigley | www.manigley.ch |
Mitsubishi | www.mitsubishicarbide.com |
Sandvik Coromant | www.sandvik.coromant.com |
SECO TOOLS | www.secotools.com |
Witech | www.witec-tools.de |
WNT | www.wnt.com |
Drilling recommendations
HSS drill
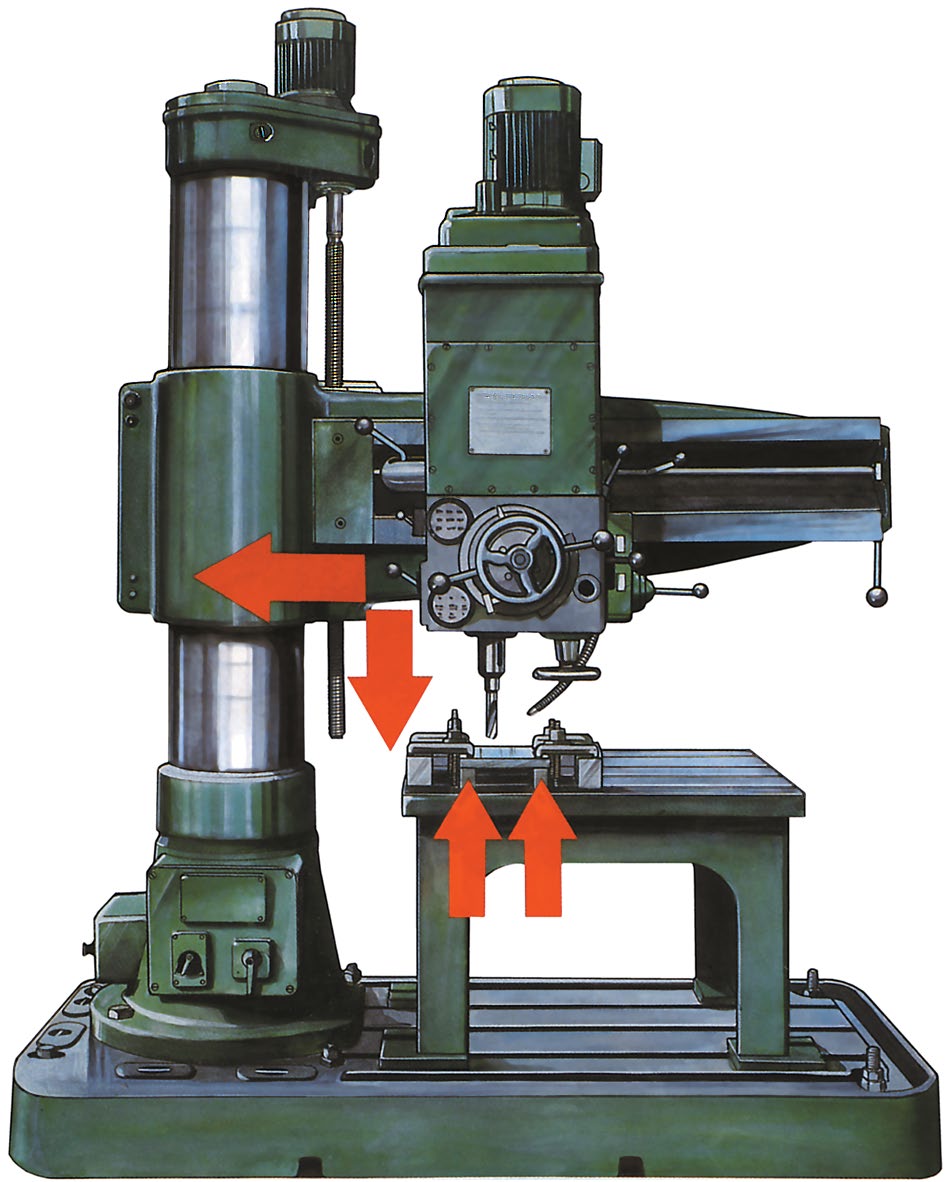
Use only HSS drills when you have unstable machine conditions. HSS drills are only suitable up to 500 Brinell. If the machine conditions are good you have several choices of solid cemented carbide drills, drills with exchangeable heads or indexable insert drills.
Advice for reducing vibrations and increasing the lifetime of the drill
- Minimize the distance to the column and between the drill tip and the workpiece.
- Don't use a longer drill than necessary.
- Always use metal supports and clamp the workpiece securely.
- Use a solid and stable table.
- Always use coolant, with a coolant mix of 8-10%.
- Just before the drill breaks through, disengage the feed rate for about a second — play and springback can otherwise snap the drill tip. Re-engage the feed rate once the play has ceased.
HSS, HSS-E, HSS-Co
Individual holes can be drilled with an ordinary HSS drill. For rational production, either a microalloyed (HSS-E) drill or a cobalt-alloyed (HSS-Co) drill is recommended. Use an HSS-Co drill (8% Co) with a small helix angle and a robust core that can withstand high torques.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | ~ 18 | ~ 15 | ~ 7 | ~ 5 |
Drill Ø | Feed rate, fn (mm/rev) and speed (rpm) | |||
5 | 0.06/1150 | 0.06/950 | 0.05/445 | 0.04/280 |
10 | 0.12/570 | 0.11/475 | 0.10/220 | 0.08/140 |
15 | 0.17/380 | 0.16/320 | 0.15/150 | 0.12/95 |
20 | 0.24/290 | 0.23/240 | 0.20/110 | 0.16/70 |
25 | 0.30/230 | 0.29/190 | 0.25/90 | 0.20/55 |
30 | 0.36/190 | 0.35/160 | 0.30/75 | 0.24/45 |
Formulas and definitions
Vc = π x d x n/1000 | π = 3.14 |
n = Vc x 1000 / (π x d) | Vc = cutting speed (m/min) |
vf = n x fn | n = speed (rpm) |
fn = feed rate (mm/rev) | |
vf = feed rate (mm/min) | |
d = drill diameter |
Advice for drilling thin plate below 8 mm
- It is important to have good support under the plate to avoid deflection.
- An indexable drill is recommended, because it begins cutting at the periphery and does not build up the same high pressure as a solid carbide drill.
- With a drill diameter over Ø 10 mm and a point angle of 118-140° it is very important to support the plate that is drilled. If the drill tip breaks through the bottom surface without a supporting plate to guide the tip, it may result in an oval and undersized hole.
- Reduce feed rate and increase cutting speed Vc, especially when using an indexable drill.
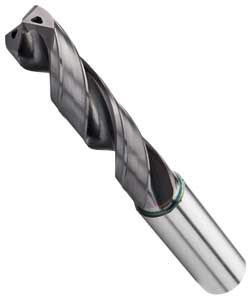
Indexable insert drill
For stable machine conditions and with internal coolant. Important: use as short a drill as possible. The recommendations are for 2×Ø.
The cutting data for indexable drills has been developed in co-operation with Sandvik Coromant.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | ||
|---|---|---|---|---|---|
Vc (m/min) | 100-150 | 80-140 | 50-90 | 40-70 | |
fn (mm/rev) | min-max | min-max | min-max | min-max | |
Diameter | 12.0-20.0 | 0.04-0.10 | 0.04-0.10 | 0.04-0.10 | 0.04-0.08 |
20.01-30.0 | 0.06-0.12 | 0.06-0.12 | 0.06-0.12 | 0.04-0.10 | |
30.01-44.0 | 0.06-0.14 | 0.06-0.14 | 0.06-0.14 | 0.06-0.12 | |
44.01-63.5 | 0.08-0.16 | 0.08-0.16 | 0.08-0.16 | 0.08-0.14 |
Drills with exchangeable drill heads
For stable machine conditions and with internal coolant.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | ||
|---|---|---|---|---|---|
Vc (m/min) | 70-100 | 60-90 | 40-60 | 35-50 | |
fn (mm/rev) | min-max | min-max | min-max | min-max | |
Diameter | 7.5-12.0 | 0.08-0.13 | 0.08-0.13 | 0.07-0.11 | 0.06-0.10 |
12.01-20.0 | 0.13-0.22 | 0.13-0.22 | 0.11-0.15 | 0.10-0.14 | |
20.01-25.0 | 0.22-0.28 | 0.22-0.27 | 0.15-0.20 | 0.14-0.18 | |
25.01-33.0 | 0.28-0.37 | 0.27-0.36 | 0.20-0.28 | 0.18-0.24 |
Solid cemented carbide drill
For stable machine conditions and with internal coolant.
- Drilling 7 × Dc: reduce the feed rate by approximately 20%.
- Drilling with external coolant: reduce the speed and feed rate by approximately 20%.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | ||
|---|---|---|---|---|---|
Vc (m/min) | 70-100 | 60-90 | 40-60 | 35-50 | |
fn (mm/rev) | min-max | min-max | min-max | min-max | |
Diameter | 3.0-5.0 | 0.03-0.06 | 0.03-0.06 | 0.03-0.05 | 0.03-0.05 |
5.01-10.0 | 0.06-0.12 | 0.06-0.12 | 0.05-0.11 | 0.05-0.10 | |
10.01-15.0 | 0.12-0.18 | 0.12-0.18 | 0.11-0.16 | 0.10-0.15 | |
15.01-20.0 | 0.18-0.25 | 0.18-0.24 | 0.16-0.22 | 0.15-0.19 |
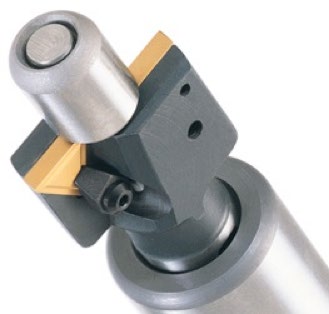
Countersinking and counterboring recommendations
Countersinking and counterboring is best performed using tools with replaceable inserts from the tool supplier Granlund. Always use a rotating pilot and use coolant. See the table below for the tool article number and corresponding screw size. Reduce the cutting data by about 30% for countersinking.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 70-100 | 40-80 | 20-50 | 15-45 |
fn (mm/rev) | 0.10-0.20 | 0.10-0.20 | 0.10-0.20 | 0.10-0.20 |
Diameter | Speed (rpm) | |||
18.0-26.0 | 855-1770 | 490-1415 | 245-885 | 185-795 |
26.0-38.0 | 590-1225 | 335-980 | 170-610 | 125-550 |
38.0-47.0 | 475-840 | 270-670 | 135-420 | 100-380 |
47.0-60.0 | 370-680 | 210-540 | 105-340 | 80-305 |
Countersinking and counterboring table for screws
Size | Article number | Ø screw head |
|---|---|---|
M8 | 0KV9-18.0 | 16 |
M10 | 0KV9- 20.5 / 1KV9- 20.0 | 20 |
M12 | 0KV9- 25.0 / 1KV9- 26.0 | 24 |
M14 | 1KV9- 30.0 | 27 |
M16 | 1KV9- 30.0 / 2KV9- 32.0 | 30 |
M20 | 2KV9- 38.0 | 36 |
M24 | 2KV9- 40.0 | 39 |
Size | Article number | Ø screw head |
|---|---|---|
M10 | 0WHV- 18.0 | 16 |
M12 | 0WHV- 20.0 / 1WHV- 20.0 | 18 |
M14 | 0WHV- 23.0 / 1WHV- 23.0 | 21 |
M16 | 1WHV- 26.0 | 24 |
M20 | 1WHV- 32.0 | 30 |
M24 | 1WHV- 38.0 / 2WHV- 38.0 | 36 |
M30 | 2WHV-47.0 | 45 |
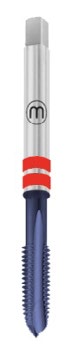
Tapping recommendations
With correct tools and tool holders we recommend tapping up to 500 Brinell with four-flute taps that can withstand the very high torque occurring during tapping in hard materials. If diameter is not critical, the drilled hole can be 3% larger than standard (see the table below). This will increase the lifetime of the tap.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 10-12 | 7-10 | 3-5 | 2.5-3.5 |
Size | Speed (rpm) | |||
M5 | 635-765 | 445-635 | -* | -* |
M6 | 530-640 | 370-530 | 210-320 | -* |
M8 | 400-480 | 280-400 | 160-240 | 100-140 |
M10 | 320-380 | 225-320 | 125-190 | 80-110 |
M12 | 265-320 | 185-265 | 105-160 | 65-95 |
M14 | 225-275 | 160-225 | 90-135 | 57-80 |
M16 | 200-240 | 140-200 | 80-120 | 50-70 |
M20 | 160-190 | 110-160 | 65-95 | 40-55 |
M24 | 130-160 | 90-135 | 50-80 | 30-45 |
M27 | 120-140 | 80-120 | 45-70 | 30-40 |
M30 | 105-125 | 75-105 | 40-65 | 25-35 |
* Tapping is not suitable. We recommend thread milling.
Emuge Franken is one tool supplier that has the type of tool holders we recommend for tapping.
Size | Pitch | Drill Ø min-max |
|---|---|---|
M4 | 0.7 | 3.3-3.4 |
M5 | 0.8 | 4.2-4.3 |
M6 | 1 | 5.0-5.1 |
M8 | 1.25 | 6.8-6.9 |
M10 | 1.5 | 8.5-8.7 |
M12 | 1.75 | 10.25-10.5 |
M14 | 2 | 12-12.3 |
M16 | 2 | 14-14.3 |
M20 | 2.5 | 17.5-18 |
M24 | 3 | 21-21.5 |
M27 | 3 | 24-24.5 |
M30 | 3.5 | 26.5-27.0 |
Thread milling recommendations
A CNC machine is necessary for thread milling. The tool supplier can provide programming support for the CNC machines.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 100-130 | 80-110 | 50-70 | 40-60 |
fz (mm/tooth) | 0.03-0.06 | 0.03-0.06 | 0.02-0.05 | 0.02-0.05 |
Tapping and thread milling advice
- Taps for blind holes have a shorter tool life due to the smaller core diameter.
- Before tapping, make sure that the predrilled hole is in good condition (don't use worn out drills).
- Always use coated taps.
- Perform thread milling in 2 passes.
- Make sure that the coolant mix is between 8-10%.
- We recommend climb milling.
Milling recommendations
Milling advice
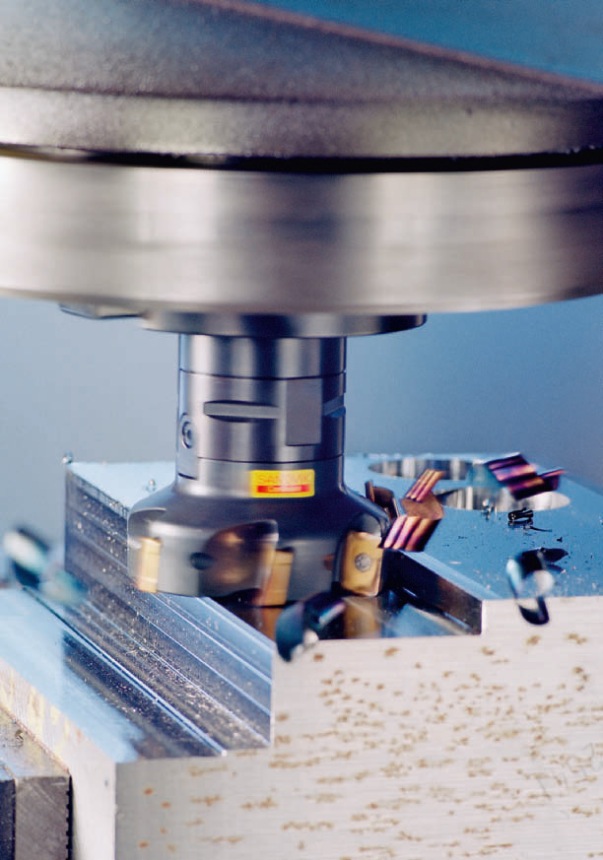
- Position the cutter off-center (to the left) to achieve a thicker chip at the entry and to avoid a thick chip at the exit.
- Avoid cutting through the center line of the cutter, as this could generate vibration.
- Always use down milling (climb milling).
- The recommendation is that the width of the cut (ae) is 25% or 75-80% of the diameter.
- Use the rolling-into-cut method.
- Dry milling is recommended if inserts are used.
- If machine power is low, use a coarse-pitch cutter.
- Always use suitable, high-quality clamping equipment.
- The depth of cut when milling gas-cut edges should be at least 2 mm, to avoid the hard surface layer of the cut edge.
If you enter the workpiece with the rolling-into-cut method the chip thickness on the exit is always zero, and it will help to give a longer tool life.
Formulas and definitions
n= Vc x1000/π x d | π = 3.14 |
Vc= π x d x n/1000 | Vc=cutting speed (m/min) |
vf =fz x n x zn | n=speed (rpm) |
fz=vf/n x zn | fz= feed rate per tooth (mm/tooth) |
vf=feed rate (mm/min) | |
zn=number of cutting edges | |
d=tool diameter | |
ap=cutting depth (mm) |
Insert grades for milling
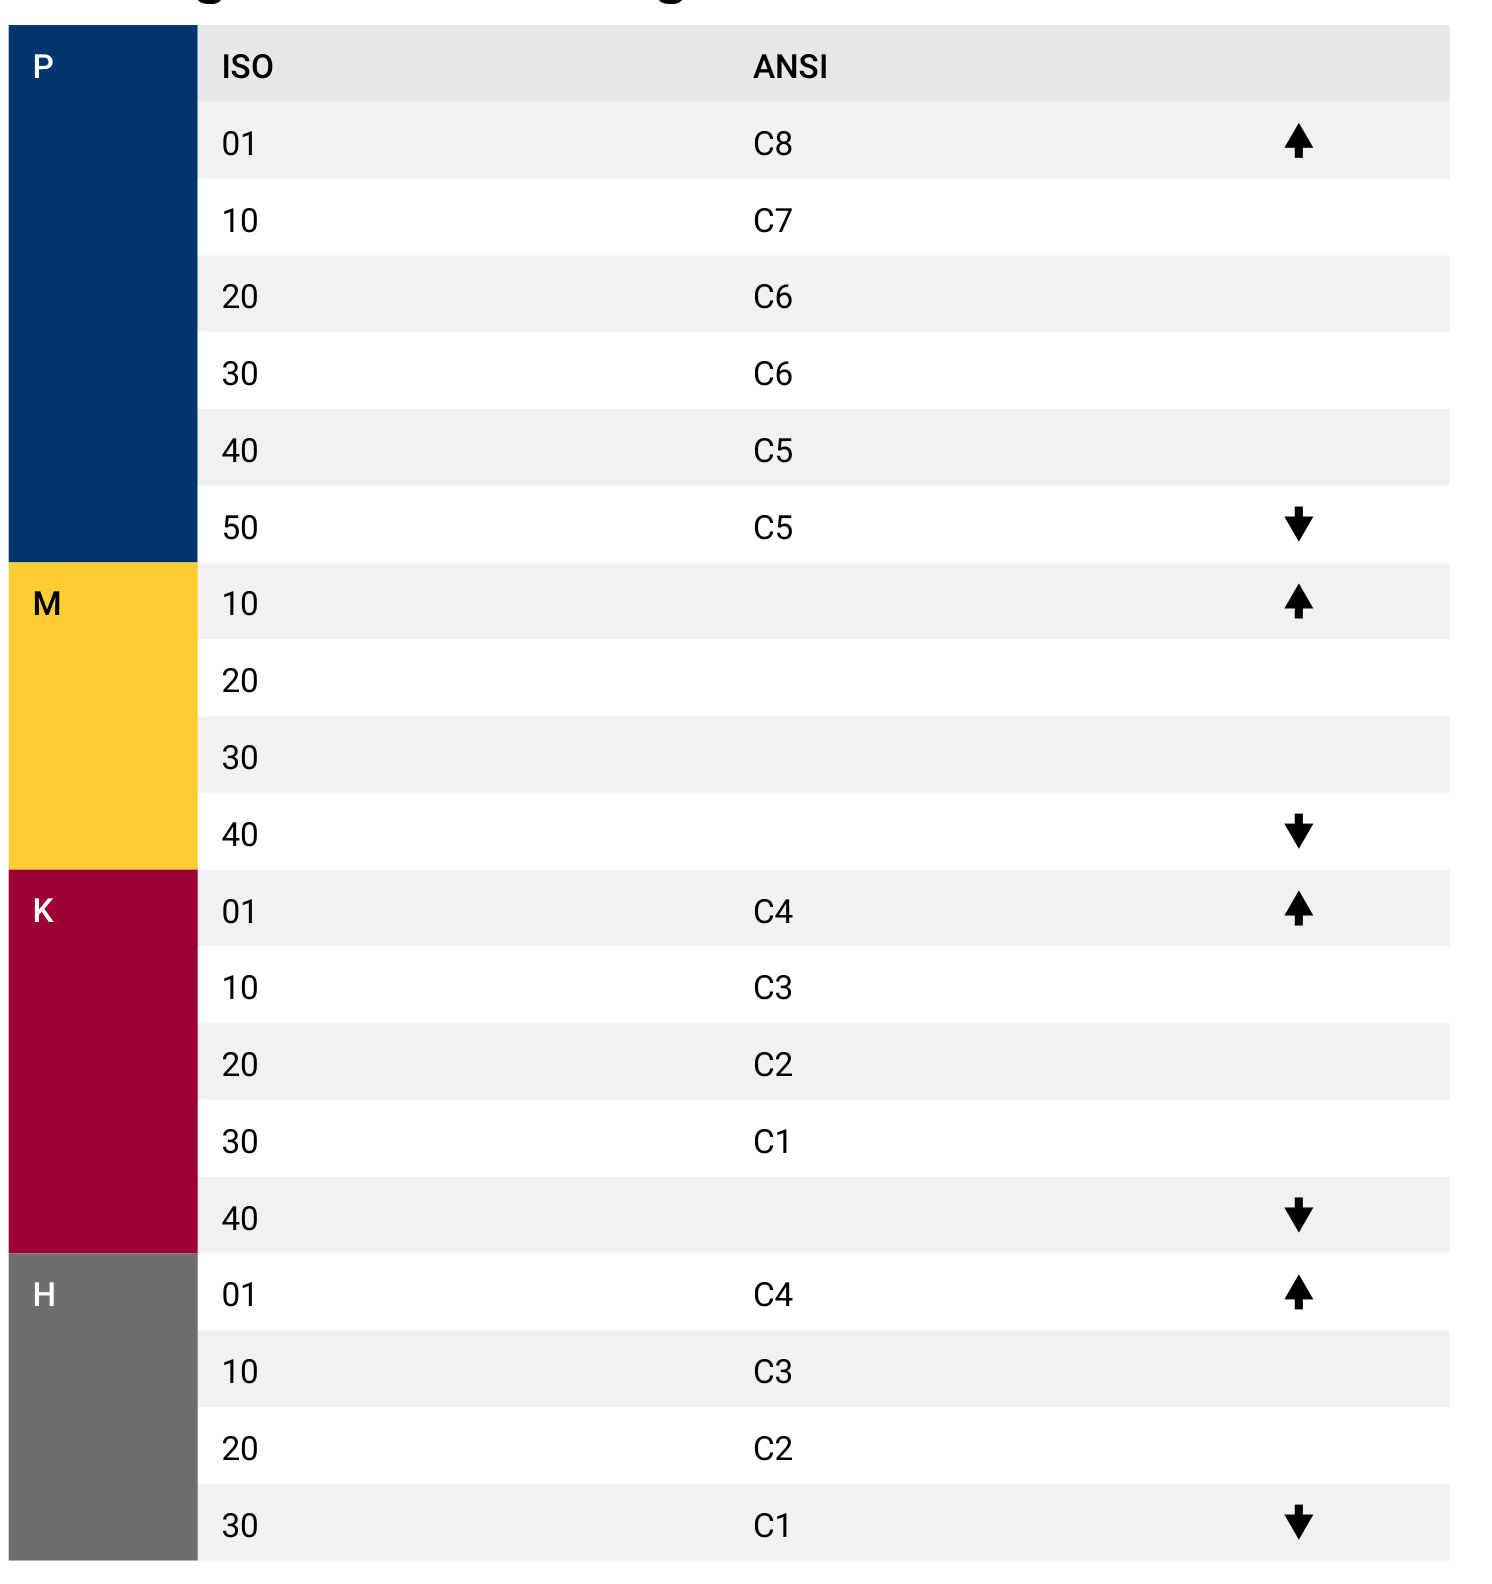
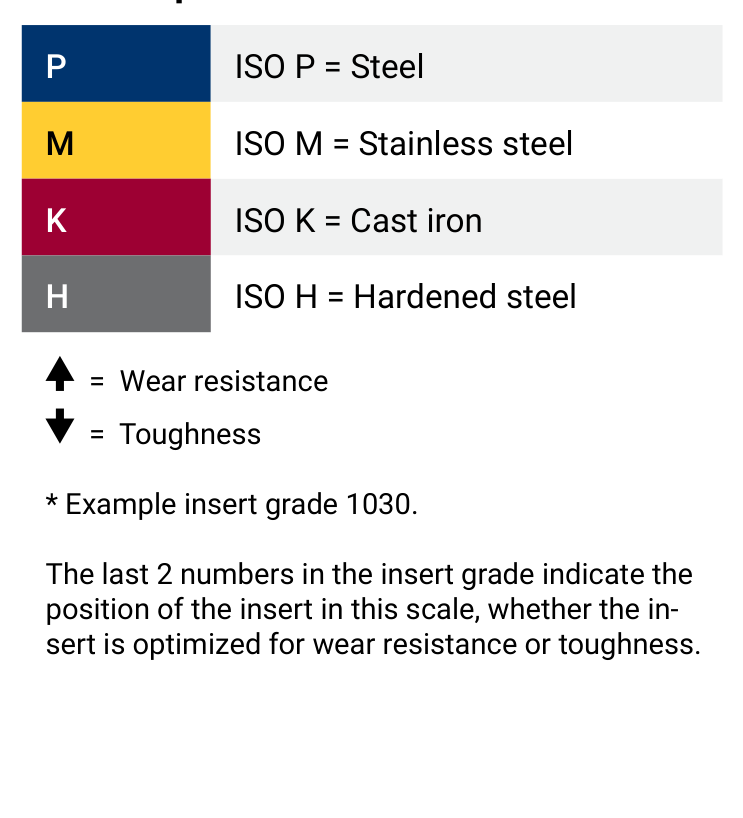
The last two numbers in the insert grade indicate the position of the insert in this scale, whether the insert is optimized for wear resistance or toughness.
Insert geometry
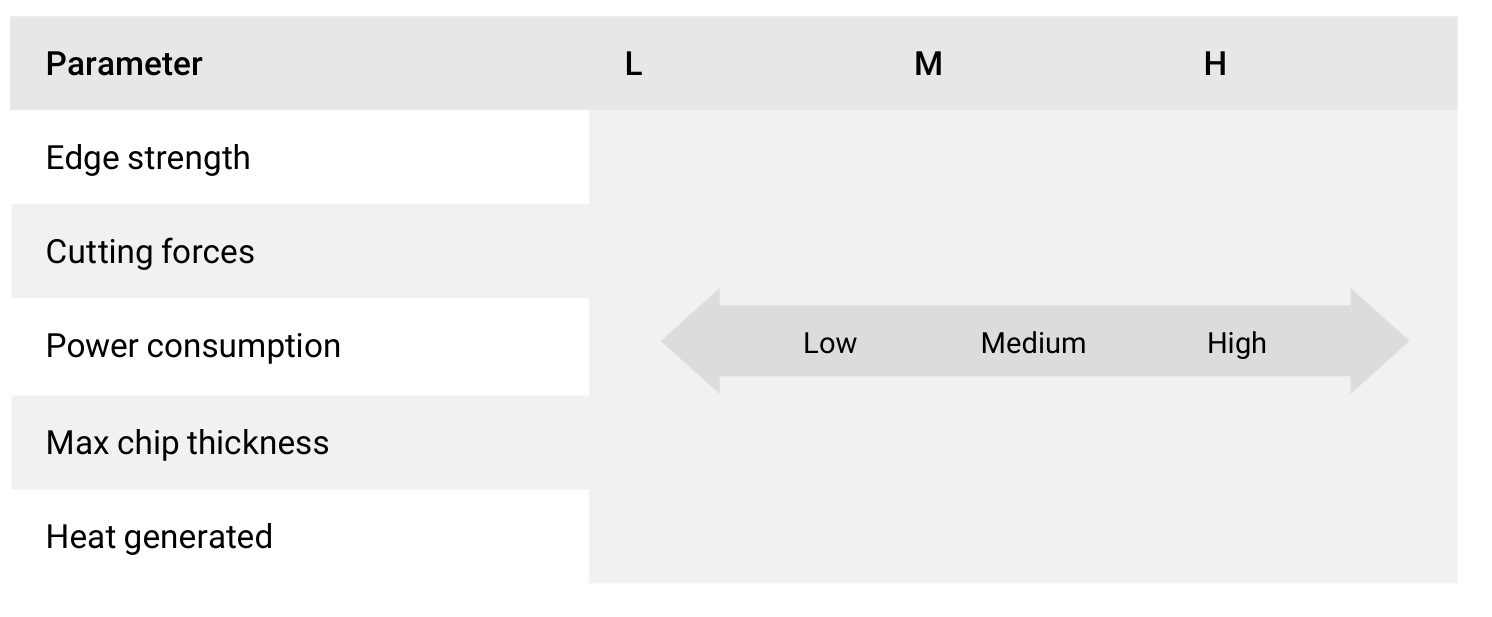
The macro geometry affects many parameters in the cutting process. An insert with a strong cutting edge can work at higher loads, but it will also generate higher cutting forces, consume more power and generate more heat.
- Use inserts grade P30-50 with light cutting geometry and a coarse-pitch cutter if the machine power is low and with unstable machine conditions.
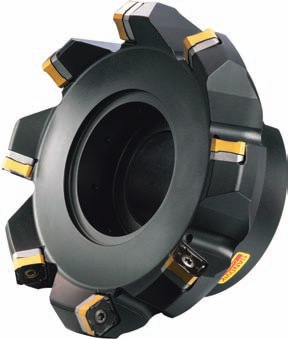
Face milling recommendation with a 45° setting angle
In very stable machine conditions and with a rigid set-up the insert grade P10 would be more suitable in all milling operations with inserts. The cutting speed can then be increased by approximately 80-100%. The data below is a recommendation for average machine conditions.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 200-250 | 180-220 | 110-150 | 100-140 |
Feed rate (fz) | min-max | min-max | min-max | min-max |
0.15-0.35 | 0.15-0.35 | 0.15-0.35 | 0.15-0.35 |
Face milling recommendation with round inserts
Round inserts have strong cutting edges and are good to use when the surface has holes and cavities. Recommendation for average machine conditions.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 200-250 | 180-220 | 110-150 | 100-140 |
Feed rate (fz) | min-max | min-max | min-max | min-max |
0.10-0.25 | 0.10-0.25 | 0.10-0.25 | 0.10-0.25 |
Shoulder milling recommendation with a 90° setting angle
Recommendation for average machine conditions.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 200-250 | 180-220 | 110-150 | 90-130 |
Feed rate (fz) | min-max | min-max | min-max | min-max |
0.12-0.25 | 0.12-0.25 | 0.12-0.25 | 0.12-0.25 |
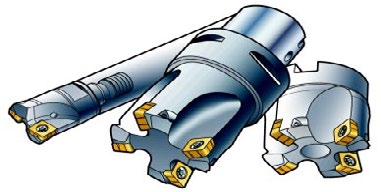
Slot milling advice
Depth of cut (ap) max 0.5 × D. End milling recommendation for a solid cemented carbide tool.
- The fz and pitch per revolution are recommendations for Coromill 210 from Sandvik Coromant.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | ||
|---|---|---|---|---|---|
Vc (m/min) | 95-120 | 85-110 | 70-95 | 45-70 | |
Feed rate (fz) | min-max | min-max | min-max | min-max | |
Diameter | 3.0-6.0 | 0.01-0.035 | 0.01-0.03 | 0.01-0.03 | 0.01-0.025 |
8.0-12.0 | 0.04-0.07 | 0.04-0.07 | 0.03-0.06 | 0.03-0.05 | |
14.0-20.0 | 0.07-0.10 | 0.07-0.10 | 0.06-0.08 | 0.05-0.07 |
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | |
|---|---|---|---|---|
Vc (m/min) | 200-250 | 180-220 | 110-150 | 100-140 |
Feed rate (fz) | min-max | min-max | min-max | min-max |
Insert grade P30 | 0.15-0.35 | 0.15-0.35 | 0.15-0.35 | 0.15-0.35 |
Shoulder milling advice
Use the whole cutting length for ap; radial depth of cut (ae) max 0.1 × D.
- If possible, use only compressed air to remove the chip, and use a Weldon chuck for tools over Ø 10 mm.
Strenx® 700 | Strenx® 900/960 | Strenx® 1100 | Strenx® 1300 | ||
|---|---|---|---|---|---|
Vc (m/min) | 210-240 | 180-210 | 160-190 | 120-150 | |
Feed rate (fz) | min-max | min-max | min-max | min-max | |
Diameter | 3.0-6.0 | 0.02-0.05 | 0.02-0.04 | 0.02-0.04 | 0.015-0.035 |
8.0-12.0 | 0.07-0.10 | 0.06-0.09 | 0.06-0.09 | 0.05-0.07 | |
14.0-20.0 | 0.10-0.14 | 0.10-0.13 | 0.10-0.12 | 0.08-0.10 |
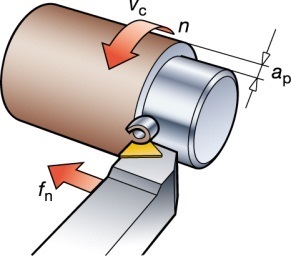
Turning recommendations
The cutting data recommendations below are applicable for tough cemented carbide grades. These grades are necessary for operations in which impact may occur, such as when turning plate with gas-cut edges.
- At higher feed rate, reduce the cutting speed.
Insert grades | P25 / C6 | P35 / C6-C7 | K20 / C2 |
|---|---|---|---|
Feed rate fn (mm/rev) | 0.1 - 0.4 - 0.8 | 0.1 - 0.4 - 0.8 | 0.1 - 0.3 |
Cutting speed Vc (m/min) | |||
Strenx® 700 | 285-195-145 | 230-150-100 | - |
Strenx® 900/960 | 130-90-70 | 105-65-45 | - |
Strenx® 1100 | 130-90-70 | 105-65-45 | - |
Strenx® 1300 | - | - | 100-80 |
Formulas and definitions
Vc = π x d x n/1000 | π = 3.14 |
n = Vc x1000/π x d | Vc = cutting speed (m/min) |
vf = n x fn | n = speed (rpm) |
fn = feed rate (mm/rev) | |
vf = feed rate (mm/min) | |
d = workpiece Ø | |
ap = cutting depth (mm) |
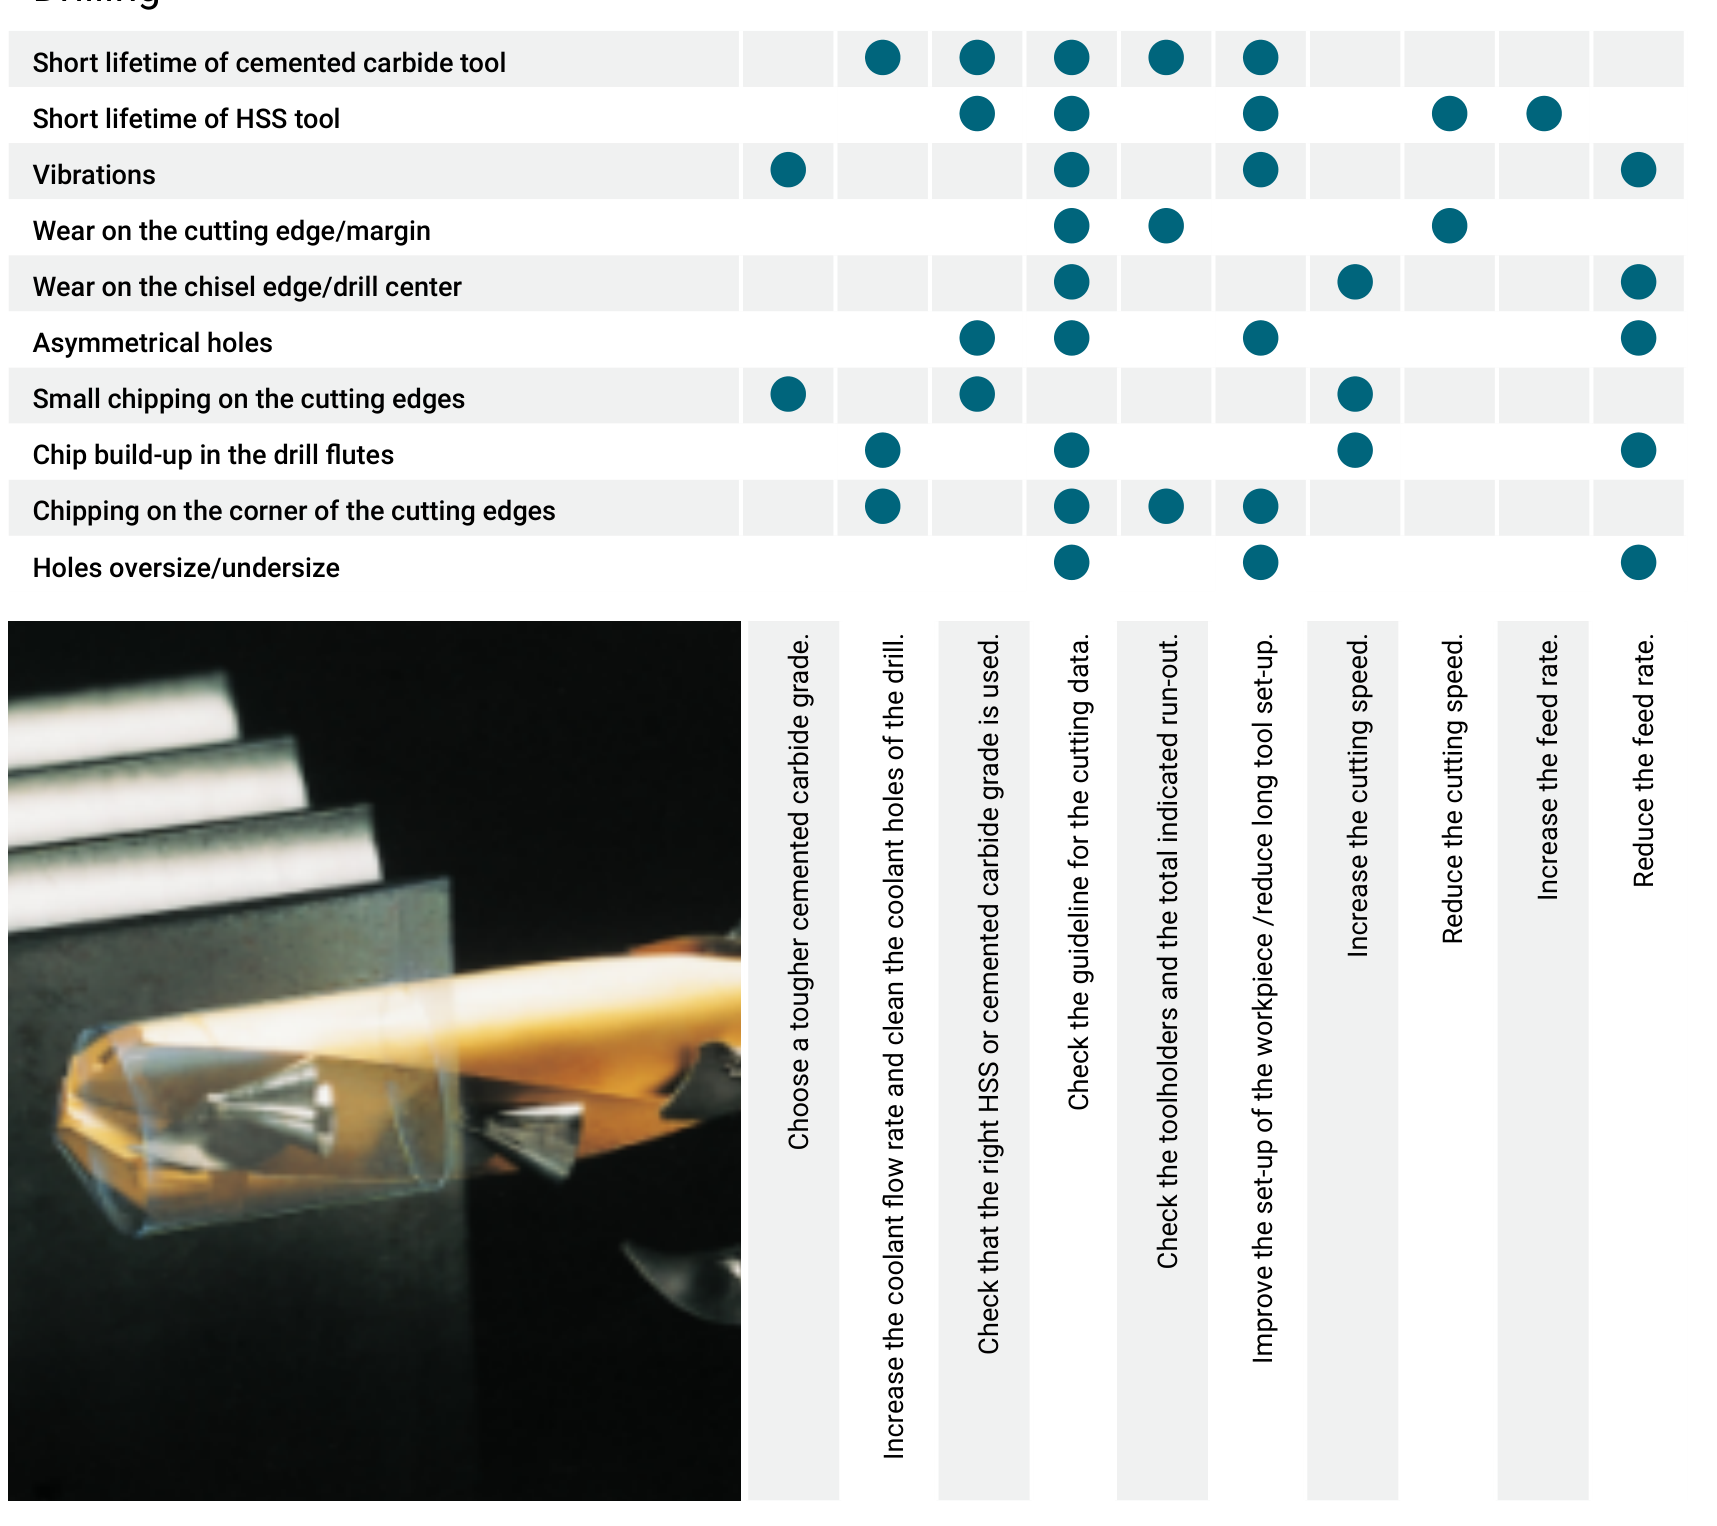
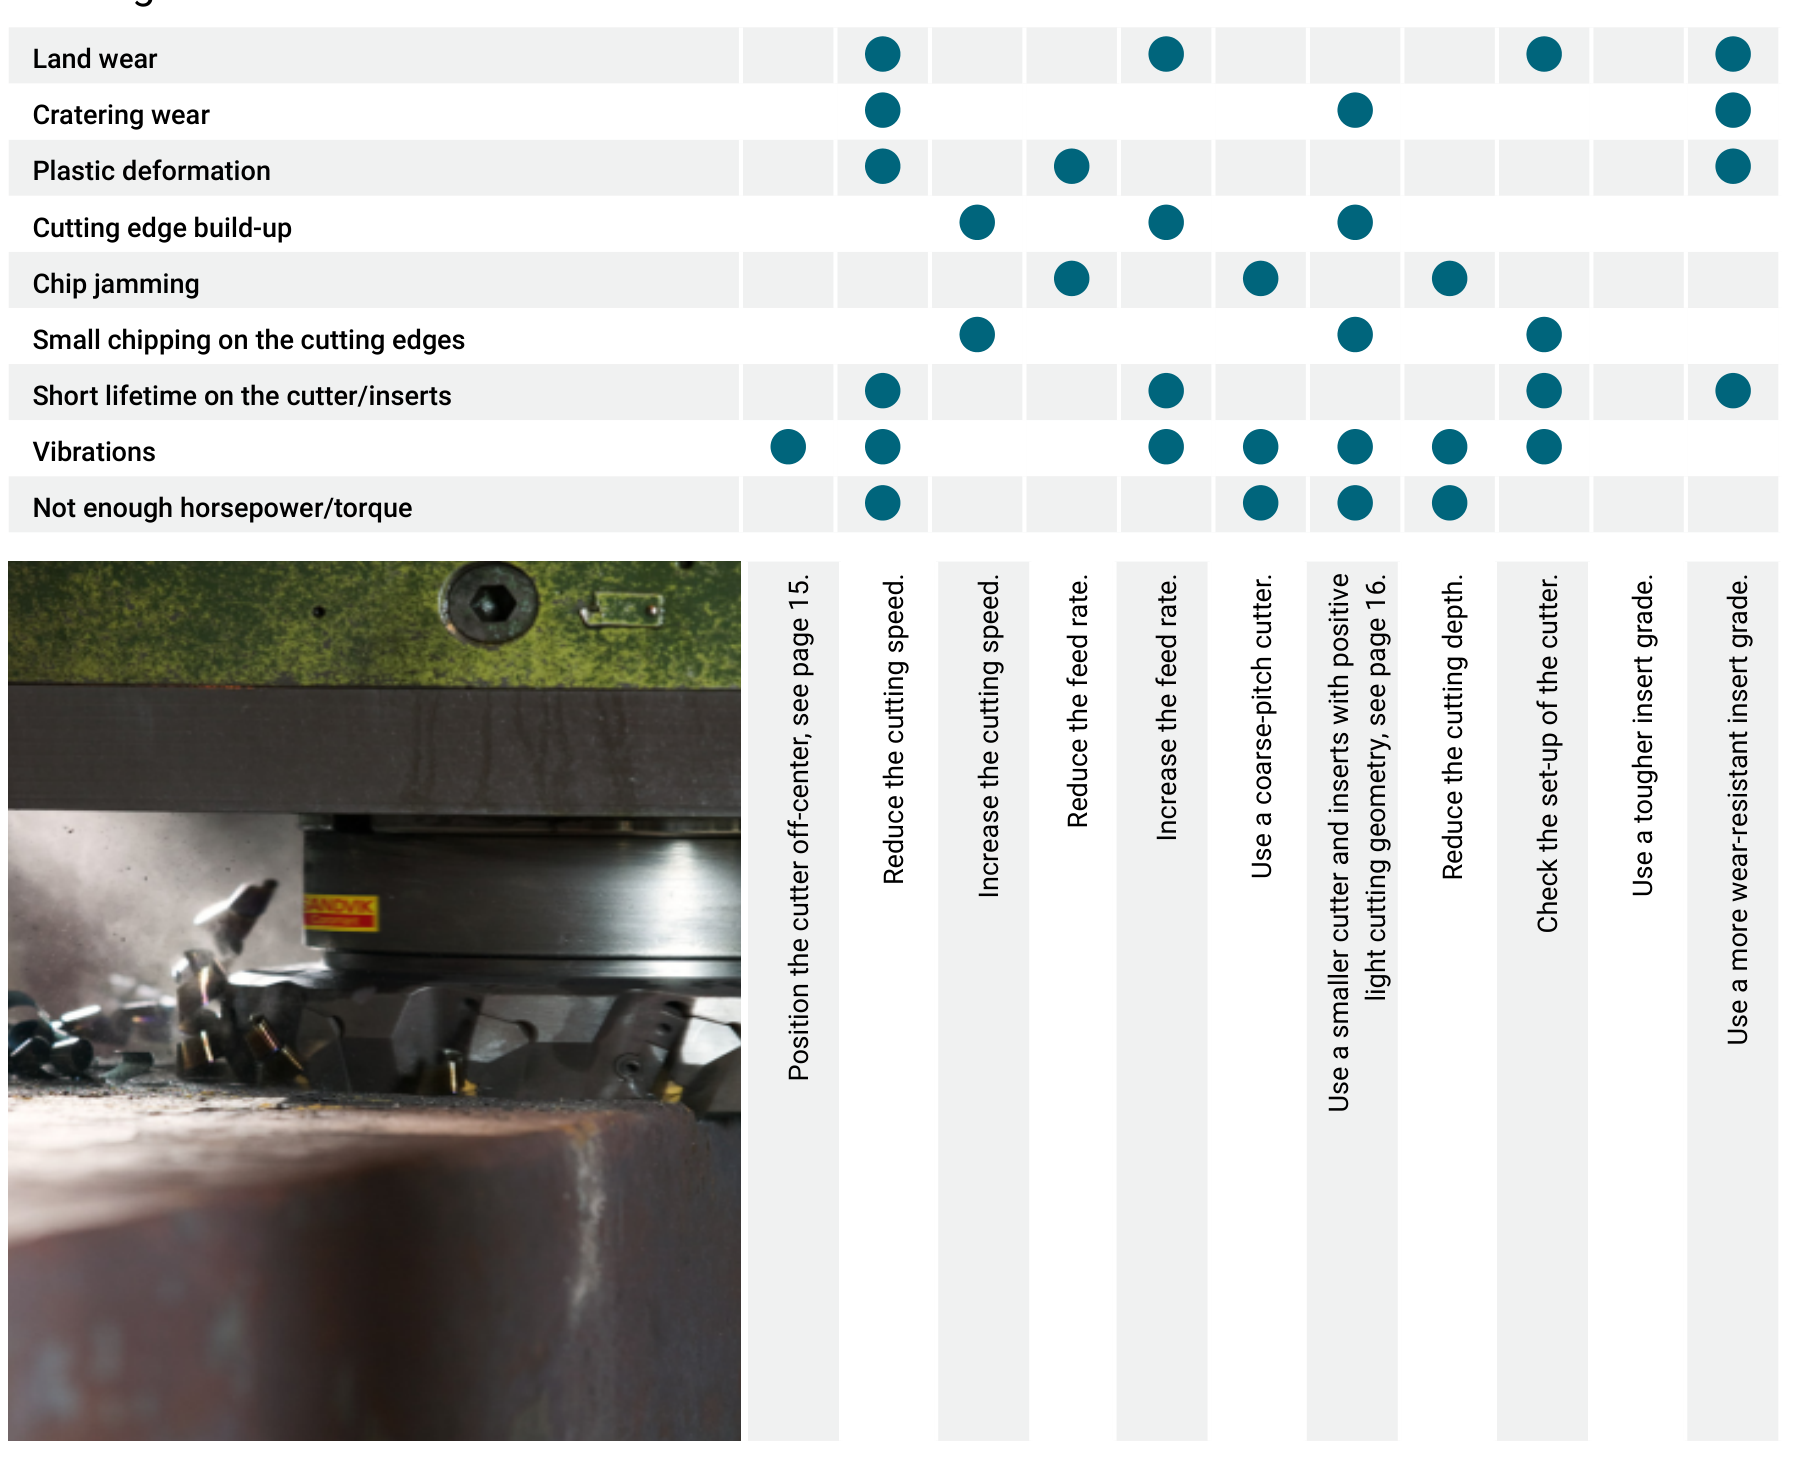
Troubleshooting for drilling and milling
The matrices below cross-reference each symptom against the remedies that apply to it — drilling first, then milling.
Tool recommendations
The tools below have been tested by SSAB together with the manufacturers. Article numbers and diameter ranges are the manufacturers' own; contact the supplier for current details.
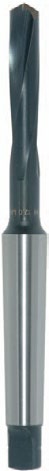
High speed steel drill alloyed with 8% cobalt (HSS-Co 8%)
Supplier: Alpen-MayKestag, Austria. www.alpenmaykestag.com
Tool name | Article number | Diameter range |
|---|---|---|
HSS -E Co 8 Taper Shank Drills, WN 103 | 832xxxxx | 8.0-40.0 |
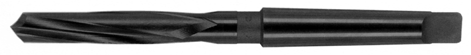
High speed steel drill alloyed with 8% cobalt (HSS-Co 8%)
Supplier: Witec, Germany. www.witec-tools.de
Tool name | Article number | Diameter range |
|---|---|---|
TYPE WITEC MN | 2-135 15 VAP | 10.0-40.0 |
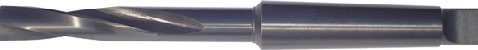
High speed steel drill alloyed with 8% cobalt (HSS-Co 8%)
Supplier: Somta, South Africa. www.somta.co.za
Tool name | Article number | Diameter range |
|---|---|---|
MTS Armour Piercing drill | 261xxxx | 10.0-50.0 |
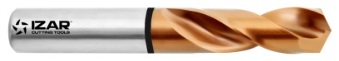
High speed steel drill alloyed with cobalt
Supplier: Izar, Spain. www.izartool.com
Tool name | Article number | Diameter range |
|---|---|---|
Ref 1054 | 32xxx | 2.0-12.0 |
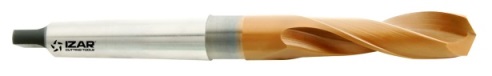
High speed steel drill alloyed with cobalt
(DRILL BIT COBALT”S”+ X-ALCR TAPER STUB). Supplier: Izar, Spain. www.izartool.com
Tool name | Article number | Diameter range |
|---|---|---|
Ref 1054 | xxxxxx | 14.0-30.0 |
High speed steel drill alloyed with 8% cobalt
(HSCo - 8%) Supplier: Presto tools, England. www.presto-tools.co.uk
Tool name | Article number | Diameter range |
|---|---|---|
Armour Piercing drill (APX) | 11211 xx.xx | 5.0-32.0 |
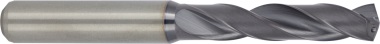
Solid cemented carbide drill
Supplier: Emuge Franken, Germany. www.emuge.de/english
Tool name | Article number | Diameter range |
|---|---|---|
EF-Drill-STEEL | TA203344.xxxx | 2.8-16.0 |
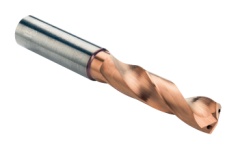
Solid cemented carbide drill
Supplier: Sandvik Coromant AB, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
Cordrill R840 Delta C | R840-xxxx-30-A1A | 3.0-20.0 |
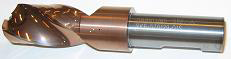
Solid cemented carbide drill
Supplier: Granlund Tool AB, Sweden. www.granlund.com
Tool name | Article number | Diameter range |
|---|---|---|
THUNDER / T80 | T80-xx.x | 10.0-30.0 |
Solid cemented carbide drill
Supplier: Mitsubishi, Japan. www.mitsubishicarbide.com
Tool name | Article number | Diameter range |
|---|---|---|
MPS1 (DP 1021) | MPS1-xxxxS | 3.0-20.0 |
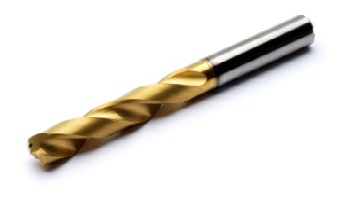
Solid cemented carbide drill
For hardness grade 450 Brinell and below, otherwise M-geometry. Supplier: Seco, Sweden. www.secotools.com
Tool name | Article number | Diameter range |
|---|---|---|
Seco Feedmax | * SD203A-12,0-36-12R1 | 2.0-20.0 |
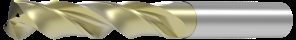
Solid cemented carbide drill
Supplier: WNT, Germany. www.wnt.com
Tool name | Article number | Diameter range |
|---|---|---|
WTX-UNI | 11780 | 3.0-25.0 |
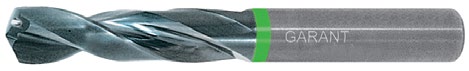
Solid cemented carbide drill
Supplier: Hoffmann-Group, Germany. www.hoffmann-group.com
Tool name | Article number | Diameter range |
|---|---|---|
Garant 122500 | 122500 | 1.0-20.0 |
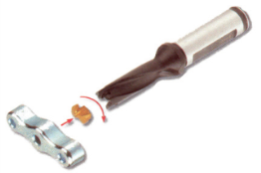
Drill with exchangeable drill heads
Drill head grade: IDI SG IC908. Supplier: Iscar, Israel. www.iscar.com
Tool name | Article number | Diameter range |
|---|---|---|
Chamdrill | DCM xxx-xxx-xxA-3D | 7.5-25.9 |
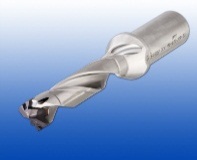
Drill with exchangeable drill heads
Drillheads grade: ICP IC 908. Supplier: Iscar, Israel. www.iscar.com
Tool name | Article number | Diameter range |
|---|---|---|
SumoCham | DCN xxx-xxx-xxA-3D | 6.0-32.0 |
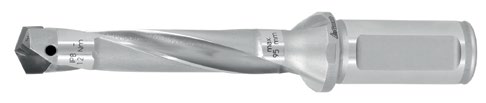
Drill with exchangeable drill heads
Drillheads grade: P-geometry (HB 7530). Supplier: Hoffmann-Group, Germany. www.hoffmann-group.com
Tool name | Article number | Diameter range |
|---|---|---|
HiPer-Drill | DCN xxx-xxx-xxA-3D | 13.0-32,75 |
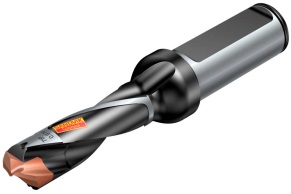
Drill with exchangeable drill heads
Drillheads grade: P-geometry (PM 4234). Supplier: Sandvik Coromant AB, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
CoroDrill 870 | 870-xxxx-xxxx | 10.0-33.0 |
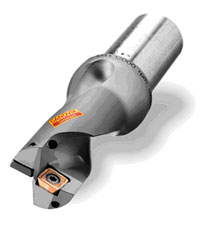
Indexable insert drill
Insert grade: Center insert LM 1044. Peripheral insert LM 4044 Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
CoroDrill 880 | 880-Dxxxxxxx-xx | 12.0-63.0 |
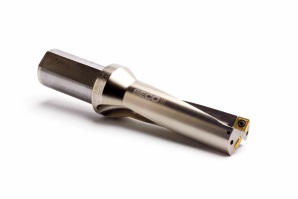
Indexable insert drill
Insert grade: T250D with P1 geometry Supplier: Seco, Sweden. www.secotools.com
Tool name | Article number | Diameter range |
|---|---|---|
Perfomax | SD503-xx.x-xxR7 | 15.0-59.0 |
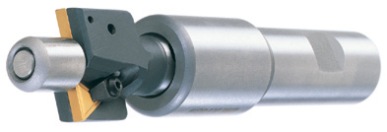
Counterboring in Strenx®
Use a counterbore with indexable inserts, and make sure the insert grade always ends with H. Supplier: Granlund Tool, Sweden. www.granlund.com
Tool name | Article number | Diameter range |
|---|---|---|
WHV counterbore | XWHV-xx.x | 18.0-75.0 |
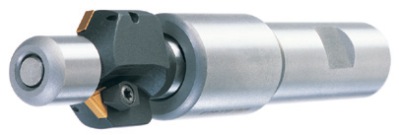
Countersinking in Strenx®
Use countersink with indexable inserts and the inserts grade should always end with H. Supplier: Granlund Tool, Sweden. www.granlund.com
Tool name | Article number | Diameter range |
|---|---|---|
KV countersink | xKV9-xx.x | 20.5-60.0 |
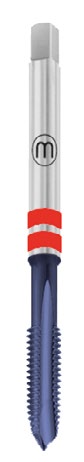
Tapping in Strenx®
Tap for through holes. HSSE-PM tap with TiCN coating Supplier: Manigley, Switzerland. www.manigley.ch
Tool name | Article number | Diameter range |
|---|---|---|
105/4 DUO | 433xx | M3-M30 |
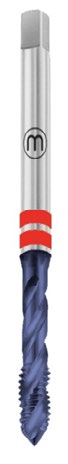
Tap for blind holes
HSSE-PM tap with TiCN coating Supplier: Manigley, Switzerland. www.manigley.ch
Tool name | Article number | Diameter range |
|---|---|---|
131/3 DUO | 433xx | M3-M36 |
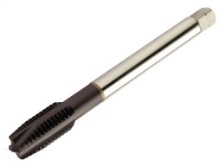
Tap for through holes
HSS-E-PM with CoolTop coating Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
CoroTap 200 | E324 / E326 | M3-M20 |
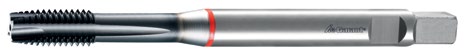
Tap for through holes
HSSE-PM with TiAlN coating Supplier: Hoffmann-Group, Germany. www.hoffmann-group.com
Tool name | Article number | Diameter range |
|---|---|---|
Garant 132065 | 132065-Mxx | M3-M16 |

Tap for through holes
HSSE-PM with TiCN coating Supplier: BASS, Germany. www.bass-tools.com
Tool name | Article number | Diameter range |
|---|---|---|
VARIANT 1/2 TIH | 1088XX | M2-M16 |
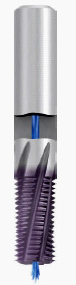
Thread milling in Strenx®
Solid carbide thread milling cutter with TiCN coating Supplier: Emuge Franken, Germany. www.emuge.de/english
Tool name | Article number | Diameter range |
|---|---|---|
GF-VZ-VHM-R15-IKZ-HB | GFB35106.xxxx | M6-M24 |
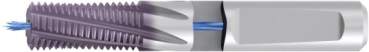
Solid carbide thread milling cutter with TiCN coating
Supplier: Emuge Franken, Germany. www.emuge.de/english
Tool name | Article number | Diameter range |
|---|---|---|
GSF-VHM 2D IKZ-HB | GF333106.xxxx | M3-M16 |
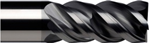
End milling in Strenx®
Solid carbide end milling cutter with Siron-A coating Supplier: Seco, Sweden. www.secotools.com
Tool name | Article number | Diameter range |
|---|---|---|
JS 554 Siron-A | JS554xxxx | 3.0-25.0 |
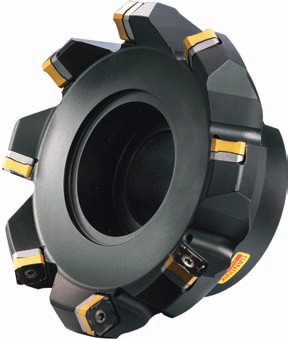
Milling with inserts in Strenx®
Face milling with Coromill 345 Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
Coromill 345 | 345-xxxxxx-13x | 40-250 |
Face milling with Coromill 300
(Round inserts) Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
Coromill 300 | R300-xxxxxx-xxx | 10-200 |
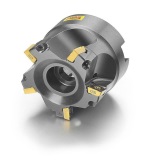
Shoulder/face milling with Coromill 490
Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
Coromill 490 | 490-xxxxx-xxx | 20-250 |
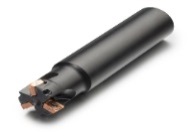
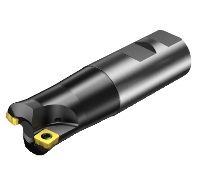
Holemaking with high feed milling
Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number | Diameter range |
|---|---|---|
Coromill 210 | R210-xxxxx-xxx | 25-160 |
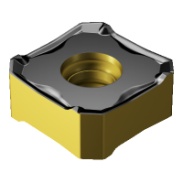
Insert grade in Strenx®
Use insert grade P1030 for average machine conditions. In very stable machines and with a rigid set-up the insert grade P1010 would be more suitable, especially over 500 Brinell. Supplier: Sandvik Coromant, Sweden. www.sandvik.coromant.com
Tool name | Article number/insert grade | Insert geometry |
|---|---|---|
Coromill 210 | R210-xxxxxxx-Px 1010 | M |
R210-xxxxxxx-Px 1030 | M | |
Coromill 300 | R300-xxxxx-Px 1010 | L-M-H |
R300-xxxxx-Px 1030 | L-M-H | |
Coromill 345 | 345R-1305x-Px 1010 | L-M-H |
345R-1305x-Px 1030 | L-M-H | |
Coromill 490 | 490R-xxxxxxx-Px 1010 | L-M |
490R-xxxxxxx-Px 1030 | L-M-H |
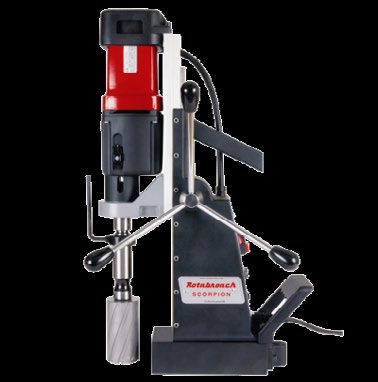
Portable magnetic drilling machines for Strenx®
Rotabroach Scorpion Supplier: Rotabroach, United Kingdom. www.rotabroach.co.uk
Model number | Type of drill | Diameter range |
|---|---|---|
Rotabroach Scorpion (Model CM 500) | TCT cutter for Strenx® (core drill) | 12-100 |
The contents of this brochure represent general suggestions. SSAB accepts no responsibility for their suitability in individual cases. The user is therefore responsible to make the necessary adaptations to the conditions in each individual case.
Source: SSAB, 421-EN Machining recommendations for Strenx®, V1 2026.