




Armox® Machining
Machining recommendations
Drilling
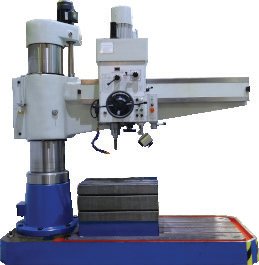
Drilling can be performed using high-speed steel drills or cemented carbide drills. When drilling in Armox® with HSS drills in radial/column drilling machines the first choice is a HSS-Co 8% drill with a small helix angle; for individual holes you can use an ordinary HSS drill.
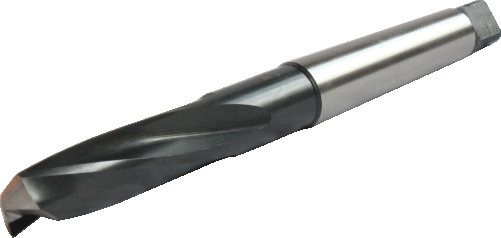
Advice for reducing vibrations and increasing the lifetime of the drill — HSS drill, max drill length 3 × diameter:
- Minimize the distances to the column and between the drill tip and the workpiece.
- Don’t use a longer drill than necessary.
- Always use metal supports.
- Clamp securely.
- Solid and firm table.
- Use coolant.
- Just before the drill breaks through, disengage the feed rate for about a second; play/spring back can otherwise snap the drill tip. Re-engage the feed rate when the play/spring back has ceased.
Table 5. HSS drill (max drill length 3 × diameter). Drill diameter (Dc) columns give the feed per revolution (fn) in mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 10 mm | Ø 15 mm | Ø 20 mm | Ø 30 mm |
|---|---|---|---|---|---|
Armox® 370T, CL 1 & 2 | 7 – 10 | 0,10 | 0,16 | 0,23 | 0,35 |
Armox® 440T | 5 – 7 | 0,09 | 0,14 | 0,20 | 0,30 |
Armox® 500T | 3 – 5 | 0,08 | 0,12 | 0,16 | 0,24 |
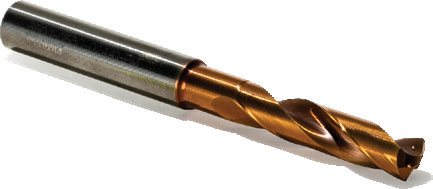
Drilling recommendations when the machine conditions are good
Solid cemented carbide drill, max drill length 3 × diameter.
Table 6. Solid cemented carbide drill (max drill length 3 × diameter). Drill diameter (Dc) columns give the feed per revolution (fn) in mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 3,0–5,0 mm | Ø 5,1–10,0 mm | Ø 10,01–15,0 mm | Ø 15,01–20,0 mm |
|---|---|---|---|---|---|
Armox® 370T, CL 1 & 2 | 60–80 | 0,03–0,06 | 0,06–0,12 | 0,12–0,17 | 0,17–0,22 |
Armox® 440T | 40–60 | 0,03–0,05 | 0,05–0,11 | 0,11–0,15 | 0,15–0,20 |
Armox® 500T | 35–60 | 0,03–0,05 | 0,05–0,10 | 0,10–0,14 | 0,14–0,18 |
Armox® 520T | 35–60 | 0,03–0,05 | 0,05–0,10 | 0,10–0,14 | 0,14–0,18 |
Armox® 560T | 30–40 | 0,03–0,05 | 0,05–0,09 | 0,09–0,13 | 0,13–0,17 |
Armox® 600T | 25–35 | 0,02–0,04 | 0,04–0,08 | 0,08–0,13 | 0,13–0,16 |
Armox® 620T | 25–35 | 0,02–0,04 | 0,04–0,08 | 0,08–0,13 | 0,13–0,16 |
Armox® Advance | 18–25 | 0,02–0,04 | 0,04–0,08 | 0,08–0,12 | 0,12–0,15 |
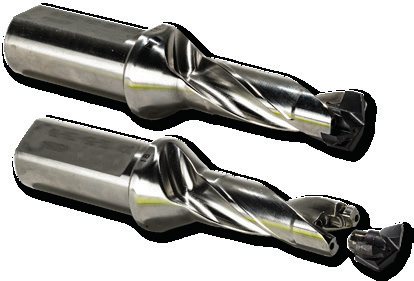
Exchangeable-tip drill, max drill length 3 × diameter.
Table 7. Exchangeable-tip drill (max drill length 3 × diameter). Feed per revolution (fn) in mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 12,0–20,0 mm | Ø 20,1–30,0 mm | Ø 30,01–44,0 mm | Ø 44,01–63,0 mm |
|---|---|---|---|---|---|
Armox® 370T, CL 1 & 2 | 60–120 | 0,04–0,10 | 0,06–0,12 | 0,06–0,14 | 0,08–0,16 |
Armox® 440T | 50–90 | 0,04–0,10 | 0,06–0,12 | 0,06–0,14 | 0,08–0,16 |
Armox® 500T | 40–70 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 520T | 40–70 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 560T | 35–55 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 600T | 30–50 | 0,04–0,06 | 0,04–0,08 | 0,06–0,10 | 0,06–0,12 |
Armox® 620T | 30–50 | 0,04–0,06 | 0,04–0,08 | 0,06–0,10 | 0,06–0,12 |
Table 8. Indexable insert drill (max drill length 2 × diameter). Feed per revolution (fn) in mm/rev. The brochure prints the same values here as in Table 7.
Steel grade | Cutting speed (Vc), m/min | Ø 12,0–20,0 mm | Ø 20,01–30,0 mm | Ø 30,01–44,0 mm | Ø 44,01–63,0 mm |
|---|---|---|---|---|---|
Armox® 370T, CL 1 & 2 | 60–120 | 0,04–0,10 | 0,06–0,12 | 0,06–0,14 | 0,08–0,16 |
Armox® 440T | 50–90 | 0,04–0,10 | 0,06–0,12 | 0,06–0,14 | 0,08–0,16 |
Armox® 500T | 40–70 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 520T | 40–70 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 560T | 35–55 | 0,04–0,08 | 0,04–0,10 | 0,06–0,12 | 0,08–0,14 |
Armox® 600T | 30–50 | 0,04–0,06 | 0,04–0,08 | 0,06–0,10 | 0,06–0,12 |
Armox® 620T | 30–50 | 0,04–0,06 | 0,04–0,08 | 0,06–0,10 | 0,06–0,12 |
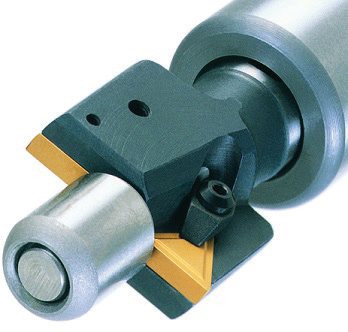
Countersinking and counterboring
Countersinking and counterboring are best performed using tools which have replaceable inserts. Always use a revolving pilot and use coolant.
Table 9. Counterboring and countersinking (tool supplier: Granlund Tools). Counterbore diameter (Dc) columns give the feed per revolution (fn) in mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 18,0–26,0 mm | Ø 26,00–38,0 mm | Ø 38,00–47,0 mm | Ø 47,00–60,0 mm |
|---|---|---|---|---|---|
Armox® 370T, CL 1 & 2 | 20–80 | 0,10–0,20 | 0,10–0,20 | 0,06–0,14 | 0,08–0,16 |
Armox® 440T | 20–50 | 0,10–0,20 | 0,10–0,20 | 0,06–0,14 | 0,08–0,16 |
Armox® 500T | 15–45 | 0,10–0,20 | 0,10–0,20 | 0,06–0,12 | 0,08–0,14 |
Armox® 520T | 15–45 | 0,10–0,20 | 0,10–0,20 | 0,06–0,12 | 0,08–0,14 |
Armox® 560T | 10–40 | 0,10–0,20 | 0,10–0,20 | 0,06–0,12 | 0,08–0,14 |
Armox® 600T | 10–35 | 0,10–0,20 | 0,10–0,20 | 0,06–0,10 | 0,06–0,12 |
Armox® 620T | 10–35 | 0,10–0,20 | 0,10–0,20 | 0,06–0,10 | 0,06–0,12 |
Important: reduce the cutting data by about 30 % for countersinking.
Milling
To ensure rational production, milling cutters with cemented carbide inserts are recommended. Keep this in mind:
- Position the cutter off-centre (to the left) to achieve a thicker chip at the entry and to avoid a thick chip on the exit.
- Cutter diameter should be 20–50 % larger than the width of cut, ae.
- Avoid centring the cutter on the centre line — that will generate more vibrations.
- Always use down milling (climb milling).
Table 12. Face milling.
Steel grade | Cutting speed (Vc), m/min | Feed per tooth (fz) min, mm/tooth — insert grade P20–P30 | Feed per tooth (fz) max, mm/tooth — insert grade P20–P30 |
|---|---|---|---|
Armox® 370T, CL 1 & 2 | 100–175 | 0,1 | 0,2 |
Armox® 440T | 50–80 | 0,1 | 0,2 |
Armox® 500T | 50–70 | 0,1 | 0,2 |
Armox® 520T | 50–70 | 0,1 | 0,2 |
Armox® 560T | 35–60 | 0,1 | 0,2 |
Armox® 600T | 30–55 | 0,07 | 0,15 |
Armox® 620T | 30–55 | 0,07 | 0,15 |
Armox® Advance | 25–40 | 0,07 | 0,15 |
Tapping and thread milling
With the correct tools, all tapping and thread milling can be performed in all Armox® grades. We recommend four-flute taps which can withstand the very high torque which occurs during tapping in hard materials. If the strength is not critical, the drilled hole can be 3 % larger than standard, which will increase the lifetime of the tap.
Table 10. Tapping.
Steel grade | Cutting speed (Vc), m/min | Size from–to |
|---|---|---|
Armox® 370T, CL 1 & 2 | 1–5 | M6–M30 |
Armox® 440T | 1–5 | M8–M30 |
Armox® 500T | 1–5 | M10–M30 |
Table 11. Thread milling.
Steel grade | Cutting speed (Vc), m/min | Feed per tooth (fz), mm/tooth |
|---|---|---|
Armox® 370T, CL 1 & 2 | 40–120 | 0,02–0,05 |
Armox® 440T | 40–120 | 0,02–0,05 |
Armox® 500T | 30–60 | 0,015–0,04 |
Armox® 520T | 30–60 | 0,015–0,04 |
Armox® 560T | 30–60 | 0,005–0,025 |
Armox® 600T | 30–40 | 0,005–0,025 |
Armox® 620T | 30–40 | 0,005–0,025 |
Armox® Advance | 25–35 | 0,005–0,015 |
To manage thread milling, a CNC machine with a minimum of 3 axes is necessary and the thread should be made in two passes.
Contact and more information
Contact your local SSAB representative or Tech Support at [email protected], or visit www.ssab.com.
This leaflet contains general suggestions and calculation models. It is the responsibility of the user to adapt the recommendations contained herein to the requirements of individual applications.