




Hardox® Machining
Machining recommendations for Hardox®
All Hardox® wear plate steel grades can be machined with high speed steel (HSS) or cemented carbide (CC) tools. This brochure contains our suggestions for cutting data (feeds and speeds) and the selection of tools. Other factors that should be taken into account in machining operations are also discussed.
Our recommendations are based on our own tests on tools of various makes and in consultation with leading tool manufacturers.
Typical properties for Hardox®. Hardness and typical yield strength by grade.
Steel grade | Hardness in Brinell (HBW) Min - Max | Typical hardness in Rockwell-C (HRC) | Typical yield strength (MPa), not guaranteed |
|---|---|---|---|
Hardox® HiTemp | 375 – 425 | - | ≈1100 |
Hardox® HiAce | 425 – 475 | - | ≈1250 |
Hardox® HiTuf | 310 – 370 | - | ≈850 |
Hardox® 400 | 370 – 430 | - | ≈1100 |
Hardox® 450 | 410 – 475 | - | ≈1250 |
Hardox® 500 | 450 – 540 | - | ≈1400 |
Hardox® 500 Tuf | 475 – 505 | - | ≈1250 - 1400 |
Hardox® 550 | 525 – 575 | - | - |
Hardox® 600 | 550 – 640 | - | - |
Hardox® Extreme | - | 57 – 63 | - |
Drilling recommendations
HSS drill
Use HSS drills only when you have unstable machine conditions. HSS drills are only suitable up to 500 Brinell. If the machine conditions are good, you can choose among solid cemented carbide drills, drills with exchangeable heads or indexable insert drills.
Advice for reducing vibrations and increasing the lifetime of the drill
- Minimize the distance to the column and between the drill tip and the workpiece.
- Don’t use a longer drill than necessary.
- Always use metal supports and clamp the workpiece securely.
- Solid and firm table.
- Always use coolant.
- Coolant mix 8-12%.
- Just before the drill breaks through, disengage the feed rate for about a second; play/springback can otherwise snap the drill tip. Re-engage the feed rate when the play/springback has ceased.
HSS drill. Cutting data for HSS drills, for unstable machine conditions and up to 500 Brinell. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 10 mm | Ø 15 mm | Ø 20 mm | Ø 25 mm | Ø 30 mm |
|---|---|---|---|---|---|---|
Hardox® HiTemp | 7 – 9 | 0.11 | 0.16 | 0.23 | 0.29 | 0.35 |
Hardox® HiAce | 5 – 7 | 0.10 | 0.15 | 0.20 | 0.25 | 0.30 |
Hardox® HiTuf | 10 – 12 | 0.10 | 0.16 | 0.23 | 0.29 | 0.35 |
Hardox® 400 | 7 – 9 | 0.11 | 0.16 | 0.23 | 0.29 | 0.35 |
Hardox® 450 | 5 – 7 | 0.10 | 0.15 | 0.20 | 0.25 | 0.30 |
Hardox® 500 | 3 – 5 | 0.08 | 0.12 | 0.16 | 0.20 | 0.24 |
Hardox® 500 Tuf | 3 – 5 | 0.08 | 0.12 | 0.16 | 0.20 | 0.24 |
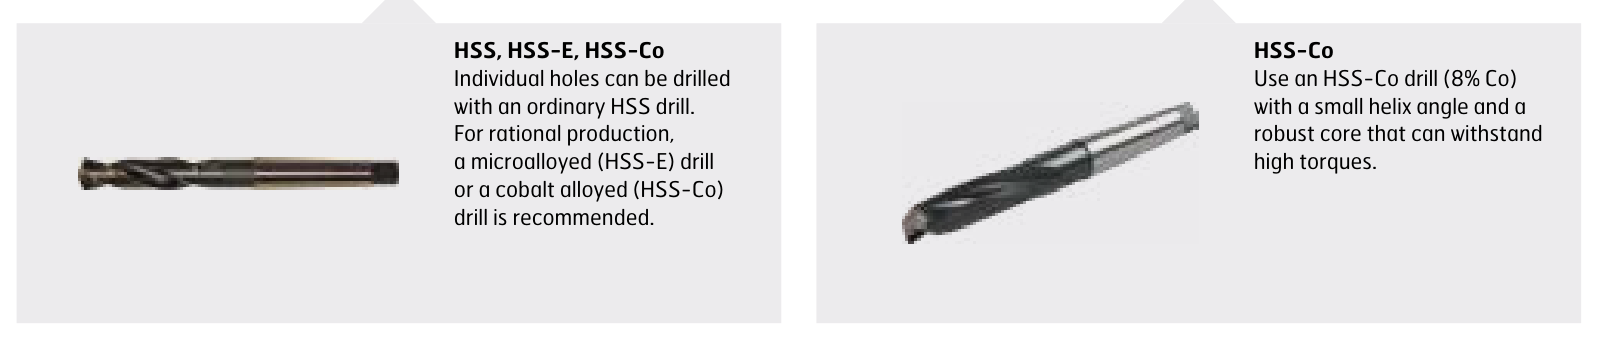
Drill choice. Individual holes can be drilled with an ordinary HSS drill; for rational production a microalloyed (HSS-E) or cobalt alloyed (HSS-Co) drill is recommended, with a small helix angle and a robust core that can withstand high torques.
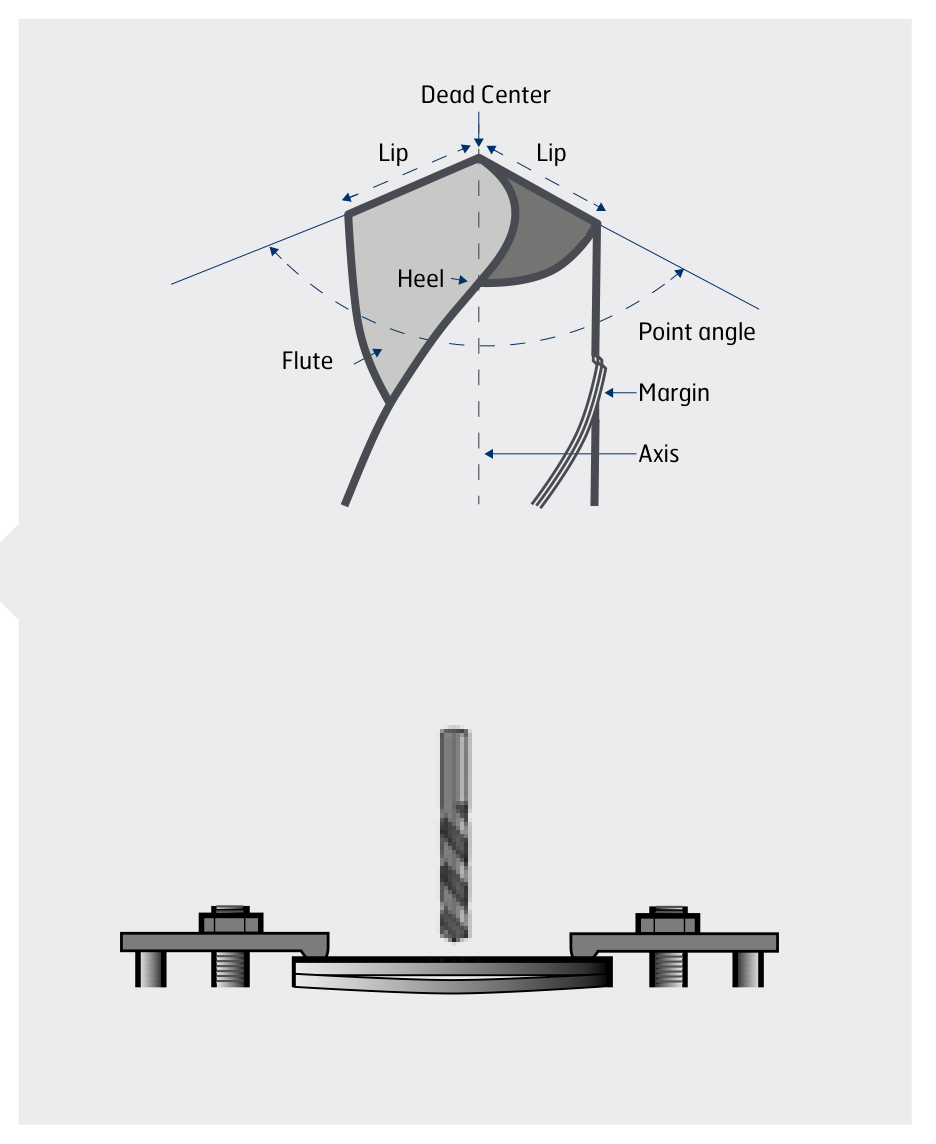
Formulas and definitions, drilling
- Vc = π × Dc × n / 1000
- n = Vc × 1000 / (π × Dc)
- Vf = fn × n
- π = 3.142
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- fn = feed per revolution (mm/r)
- Vf = penetration rate (mm/min)
- Dc = drill diameter (mm)
Advice for drilling in thin plate below 8 mm. See the panel.
Solid cemented carbide drill
For stable machine conditions and with internal coolant.
Solid cemented carbide drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 3,0 – 5,0 mm | Ø 5,01 – 10,0 mm | Ø 10,01 – 15,0 mm | Ø 15,01 – 20,0 mm |
|---|---|---|---|---|---|
Hardox® HiTemp | 50 – 70 | 0.03 – 0.06 | 0.06 – 0.12 | 0.12 – 0.16 | 0.16 – 0.21 |
Hardox® HiAce | 40 – 60 | 0.03 – 0.05 | 0.05 – 0.11 | 0.11 – 0.15 | 0.15 – 0.20 |
Hardox® HiTuf | 60 – 80 | 0.03 – 0.06 | 0.06 – 0.12 | 0.12 – 0.17 | 0.17 – 0.22 |
Hardox® 400 | 50 – 70 | 0.03 – 0.06 | 0.06 – 0.12 | 0.12 – 0.16 | 0.16 – 0.21 |
Hardox® 450 | 40 – 60 | 0.03 – 0.05 | 0.05 – 0.11 | 0.11 – 0.15 | 0.15 – 0.20 |
Hardox® 500 | 35 – 50 | 0.03 – 0.05 | 0.05 – 0.10 | 0.10 – 0.14 | 0.14 – 0.18 |
Hardox® 500 Tuf | 35 – 50 | 0.03 – 0.05 | 0.05 – 0.10 | 0.10 – 0.14 | 0.14 – 0.18 |
Hardox® 550 | 30 – 40 | 0.03 – 0.05 | 0.05 – 0.09 | 0.09 – 0.13 | 0.13 – 0.17 |
Hardox® 600 | 25 – 35 | 0.02 – 0.04 | 0.04 – 0.08 | 0.08 – 0.13 | 0.13 – 0.16 |
Hardox® Extreme | 18 – 25 | 0.02 – 0.04 | 0.04 – 0.08 | 0.08 – 0.12 | 0.12 – 0.15 |
Indexable insert drill
Indexable insert drill. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 12,0 – 20,0 mm | Ø 20,01 – 30,0 mm | Ø 30,01 – 44,0 mm | Ø 44,01 – 63,5 mm |
|---|---|---|---|---|---|
Hardox® HiTemp | 60 – 120 | 0.04 – 0.10 | 0.06 – 0.12 | 0.06 – 0.14 | 0.08 – 0.16 |
Hardox® HiAce | 50 – 90 | 0.04 – 0.10 | 0.06 – 0.12 | 0.06 – 0.14 | 0.08 – 0.16 |
Hardox® HiTuf | 70 – 130 | 0.04 – 0.10 | 0.06 – 0.12 | 0.06 – 0.14 | 0.08 – 0.16 |
Hardox® 400 | 60 – 120 | 0.04 – 0.10 | 0.06 – 0.12 | 0.06 – 0.14 | 0.08 – 0.16 |
Hardox® 450 | 50 – 90 | 0.04 – 0.10 | 0.06 – 0.12 | 0.06 – 0.14 | 0.08 – 0.16 |
Hardox® 500 | 40 – 70 | 0.04 – 0.08 | 0.04 – 0.10 | 0.06 – 0.12 | 0.08 – 0.14 |
Hardox® 500 Tuf | 40 – 70 | 0.04 – 0.08 | 0.04 – 0.10 | 0.06 – 0.12 | 0.08 – 0.14 |
Hardox® 550 | 35 – 55 | 0.04 – 0.08 | 0.04 – 0.10 | 0.06 – 0.12 | 0.08 – 0.14 |
Hardox® 600 | 30 – 50 | 0.04 – 0.06 | 0.04 – 0.08 | 0.06 – 0.10 | 0.06 – 0.12 |
Drills with exchangeable drill tip
For stable machine conditions and with internal coolant.
Drill with exchangeable drill tip. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 7,5 – 12,0 mm | Ø 12,01 – 20,0 mm | Ø 20,01 – 25,0 mm | Ø 25,01 – 33,0 mm |
|---|---|---|---|---|---|
Hardox® HiTemp | 50 – 70 | 0.08 – 0.12 | 0.12 – 0.20 | 0.20 – 0.25 | 0.25 – 0.33 |
Hardox® HiAce | 40 – 60 | 0.07 – 0.11 | 0.11 – 0.15 | 0.15 – 0.20 | 0.20 – 0.28 |
Hardox® HiTuf | 60 – 80 | 0.08 – 0.13 | 0.13 – 0.22 | 0.22 – 0.27 | 0.27 – 0.36 |
Hardox® 400 | 50 – 70 | 0.08 – 0.12 | 0.12 – 0.20 | 0.20 – 0.25 | 0.25 – 0.33 |
Hardox® 450 | 40 – 60 | 0.07 – 0.11 | 0.11 – 0.15 | 0.15 – 0.20 | 0.20 – 0.28 |
Hardox® 500 | 35 – 50 | 0.06 – 0.10 | 0.10 – 0.14 | 0.14 – 0.18 | 0.18 – 0.24 |
Hardox® 500 Tuf | 35 – 50 | 0.06 – 0.10 | 0.10 – 0.14 | 0.14 – 0.18 | 0.18 – 0.24 |
Hardox® 550 | 30 – 40 | 0.05 – 0.08 | 0.08 – 0.12 | 0.12 – 0.16 | 0.16 – 0.22 |
Hardox® 600 | 25 – 35 | 0.04 – 0.07 | 0.07 – 0.11 | 0.11 – 0.14 | 0.14 – 0.18 |
Cutting speed recommendations for Chamdrill / SumoCham in unstable machines
With this tool and with machine conditions that are not optimal, using these drills is a good solution when many holes need to be drilled. The drilling operation can be done almost 3 times faster compared to our recommendations for HSS drills. All recommendations for the cutting data are based on tests we have performed in our own radial drilling machine.
Chamdrill with exchangeable drill tip — see the tool recommendations at the end of this page. If the drill centers badly in the start, we recommend that you center the drill manually. Otherwise the drill head may break, especially with drill Ø over 15 mm.
Results from our own test. Chamdrill against HSS in a radial drilling machine.
Thickness of Hardox® 450 | Ø Drill | Vc, m/min | fn, mm/r | Nr of holes | Chamdrill vs HSS |
|---|---|---|---|---|---|
16 mm | 8.5 | 13.3 | 0.11 | 400 | 2.6 times faster |
25 mm | 14.2 | 15.8 | 0.17 | 270 | 2.6 times faster |
Thickness of Hardox® 500 | Ø Drill | Vc, m/min | fn, mm/r | Nr of holes | Chamdrill vs HSS |
12 mm | 14.2 | 11.1 | 0.11 | 300 | 2.5 times faster |
30 mm | 25 | 9.8 | 0.17 | 107 | 1.9 times faster |
Chamdrill / SumoCham in unstable machines. Cutting data by drill diameter. Columns give drill diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 7.5 – 11.5 mm | Ø 12.0 – 17.5 mm | Ø 18.0 – 25.9 mm |
|---|---|---|---|---|
Hardox® HiTemp | 12 – 22 | 0.08 – 0.12 | 0.12 – 0.18 | 0.13 – 0.24 |
Hardox® HiAce | 10 – 18 | 0.08 – 0.12 | 0.12 – 0.18 | 0.11 – 0.20 |
Hardox® HiTuf | 14 – 25 | 0.08 – 0.12 | 0.12 – 0.18 | 0.13 – 0.24 |
Hardox® 400 | 12 – 22 | 0.08 – 0.12 | 0.12 – 0.18 | 0.13 – 0.24 |
Hardox® 450 | 10 – 18 | 0.08 – 0.12 | 0.12 – 0.18 | 0.11 – 0.20 |
Hardox® 500 | 8 – 14 | 0.06 – 0.12 | 0.11 – 0.16 | 0.10 – 0.18 |
Hardox® 500 Tuf | 8 – 14 | 0.06 – 0.12 | 0.11 – 0.16 | 0.10 – 0.18 |
Countersinking and counterboring recommendations
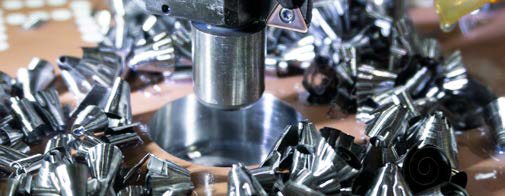
Countersinking and counterboring are best performed using tools with replaceable inserts, which are available from the tool supplier Granlund. Always use a revolving pilot and use coolant. Calculation of spindle speed uses the same formula as for drilling.
Reduce the cutting data by about 30% for countersinking.
Counterboring. Cutting data by counterbore diameter. Columns give counterbore diameter, (Dc), mm / Feed per revolution, (fn) mm/rev.
Steel grade | Cutting speed (Vc), m/min | Ø 18.0 – 26.0 mm | Ø 26.0 – 38.0 mm | Ø 38.0 – 47.0 mm | Ø 47.0 – 60.0 mm |
|---|---|---|---|---|---|
Hardox® HiTemp | 25 – 70 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® HiAce | 20 – 50 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® HiTuf | 30 – 80 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 400 | 25 – 70 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 450 | 20 – 50 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 500 | 15 – 45 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 500 Tuf | 15 – 45 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 550 | 12 – 40 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Hardox® 600 | 10 – 35 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 | 0.10 – 0.20 |
Countersinking and counterboring table for screws — KV9
Article numbers and screw head diameters for the KV9 tool series.
KV9. Tool article numbers by screw size. Image: Granlund Tools AB.
Size | Article number | Ø Screw head |
|---|---|---|
M8 | 0KV9-18.0 | 16 mm |
M10 | 0KV9- 20.5 / 1KV9- 20.0 | 20 mm |
M12 | 0KV9- 25.0 / 1KV9- 26.0 | 24 mm |
M14 | 1KV9- 30.0 | 27 mm |
M16 | 1KV9- 30.0 / 2KV9- 32.0 | 30 mm |
M20 | 2KV9- 38.0 | 36 mm |
M24 | 2KV9- 40.0 | 39 mm |
Countersinking and counterboring table for screws — WHV
Article numbers and screw head diameters for the WHV tool series.
WHV. Tool article numbers by screw size. Image: Granlund Tools AB.
Size | Article number | Ø Screw head |
|---|---|---|
M10 | 0WHV- 18.0 | 16 mm |
M12 | 0WHV- 20.0 / 1WHV- 20.0 | 18 mm |
M14 | 0WHV- 23.0 / 1WHV- 23.0 | 21 mm |
M16 | 1WHV- 26.0 | 24 mm |
M20 | 1WHV- 32.0 | 30 mm |
M24 | 1WHV- 38.0 / 2WHV- 38.0 | 36 mm |
M30 | 2WHV-47.0 | 45 mm |
Tapping recommendations
With correct tools and tool holders, we recommend tapping up to 500 Brinell with four-flute taps that can withstand the very high torque which occurs during tapping in hard materials.
Calculation of spindle speed
- n = Vc × 1000 / (π × D)
- π = 3.142
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- D = thread diameter (mm)
Tapping. Cutting speed and thread size range by grade.
Steel grade | Cutting speed (Vc), m/min | Size from - to |
|---|---|---|
Hardox® HiTemp | 4 – 8 | M6 – M30 |
Hardox® HiAce | 1 - 3 | M8 – M30 |
Hardox® HiTuf | 6 – 10 | M6 – M30 |
Hardox® 400 | 4 – 8 | M6 – M30 |
Hardox® 450 | 1 – 5 | M6 – M30 |
Hardox® 500 | 1 – 3 | M8 – M30 |
Hardox® 500 Tuf | 1 – 3 | M8 – M30 |
Tapping drill diameters. Pitch and core-hole diameter by thread size.
Size | Pitch | Drill Ø min - max |
|---|---|---|
M6 | 1 | 5.0 – 5.1 |
M8 | 1.25 | 6.8 – 6.9 |
M10 | 1.5 | 8.5 – 8.7 |
M12 | 1.75 | 10.25 – 10.5 |
M14 | 2 | 12 – 12.3 |
M16 | 2 | 14 – 14.3 |
M20 | 2.5 | 17.5 – 18 |
M24 | 3 | 21 – 21.5 |
M27 | 3 | 24 – 24.5 |
M30 | 3.5 | 26.5 – 27.0 |
Thread milling recommendations
A CNC machine is necessary for thread milling. The tool supplier can provide programming support for the CNC machines.
Thread milling. Cutting speed and feed per tooth by grade.
Steel grade | Cutting speed (Vc), m/min | Feed per tooth (fz), mm/tooth |
|---|---|---|
Hardox® HiTemp | 60 – 80 | 0.02 – 0.05 |
Hardox® HiAce | 40 – 60 | 0.02 – 0.04 |
Hardox® HiTuf | 70 – 100 | 0.03 – 0.06 |
Hardox® 400 | 60 – 80 | 0.02 – 0.05 |
Hardox® 450 | 50 – 70 | 0.02 – 0.05 |
Hardox® 500 | 40 – 60 | 0.02 – 0.05 |
Hardox® 500 Tuf | 40 – 60 | 0.02 – 0.05 |
Hardox® 550 | 35 – 55 | 0.02 – 0.04 |
Hardox® 600 | 30 – 40 | 0.01 – 0.03 |
Hardox® Extreme | 25 – 35 | 0.01 – 0.03 |
Milling recommendations
Milling advice
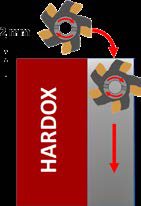
- Position the cutter off-centre (to the left) to achieve a thicker chip at the entry and to avoid a thick chip at the exit.
- Avoid cutting through the center line of the cutter, as this could generate vibration.
- Always use down milling (climb milling).
- We recommend that the width of the cut (ae) is 25 or 75-80% of the cutter diameter.
- Use the rolling into cut method.
- Dry milling is recommended if an insert is used.
- If the machine power is low use a coarse pitch cutter.
- Always use a vise or good clamping equipment.
- The depth of cut with milling gas-cut edges should be at least 2 mm, to avoid the hard surface layer of the cut edge.
- If you enter the workpiece with the rolling into cut method the chip thickness on the exit is always zero, and it will help to give a longer tool life.
Roll in to cut. The recommended entry method.
Formulas and definitions, milling
- n = Vc × 1000 / (π × Dc)
- Vc = π × Dc × n / 1000
- Vf = fz × n × Zc
- fz = Vf / (n × Zc)
- π = 3.142
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- fz = feed per tooth (mm/t)
- Vf = table feed (mm/min)
- Zc = number of effective teeth (pcs)
- Dc = cutting diameter (mm)
- ap = axial depth of cut (mm)
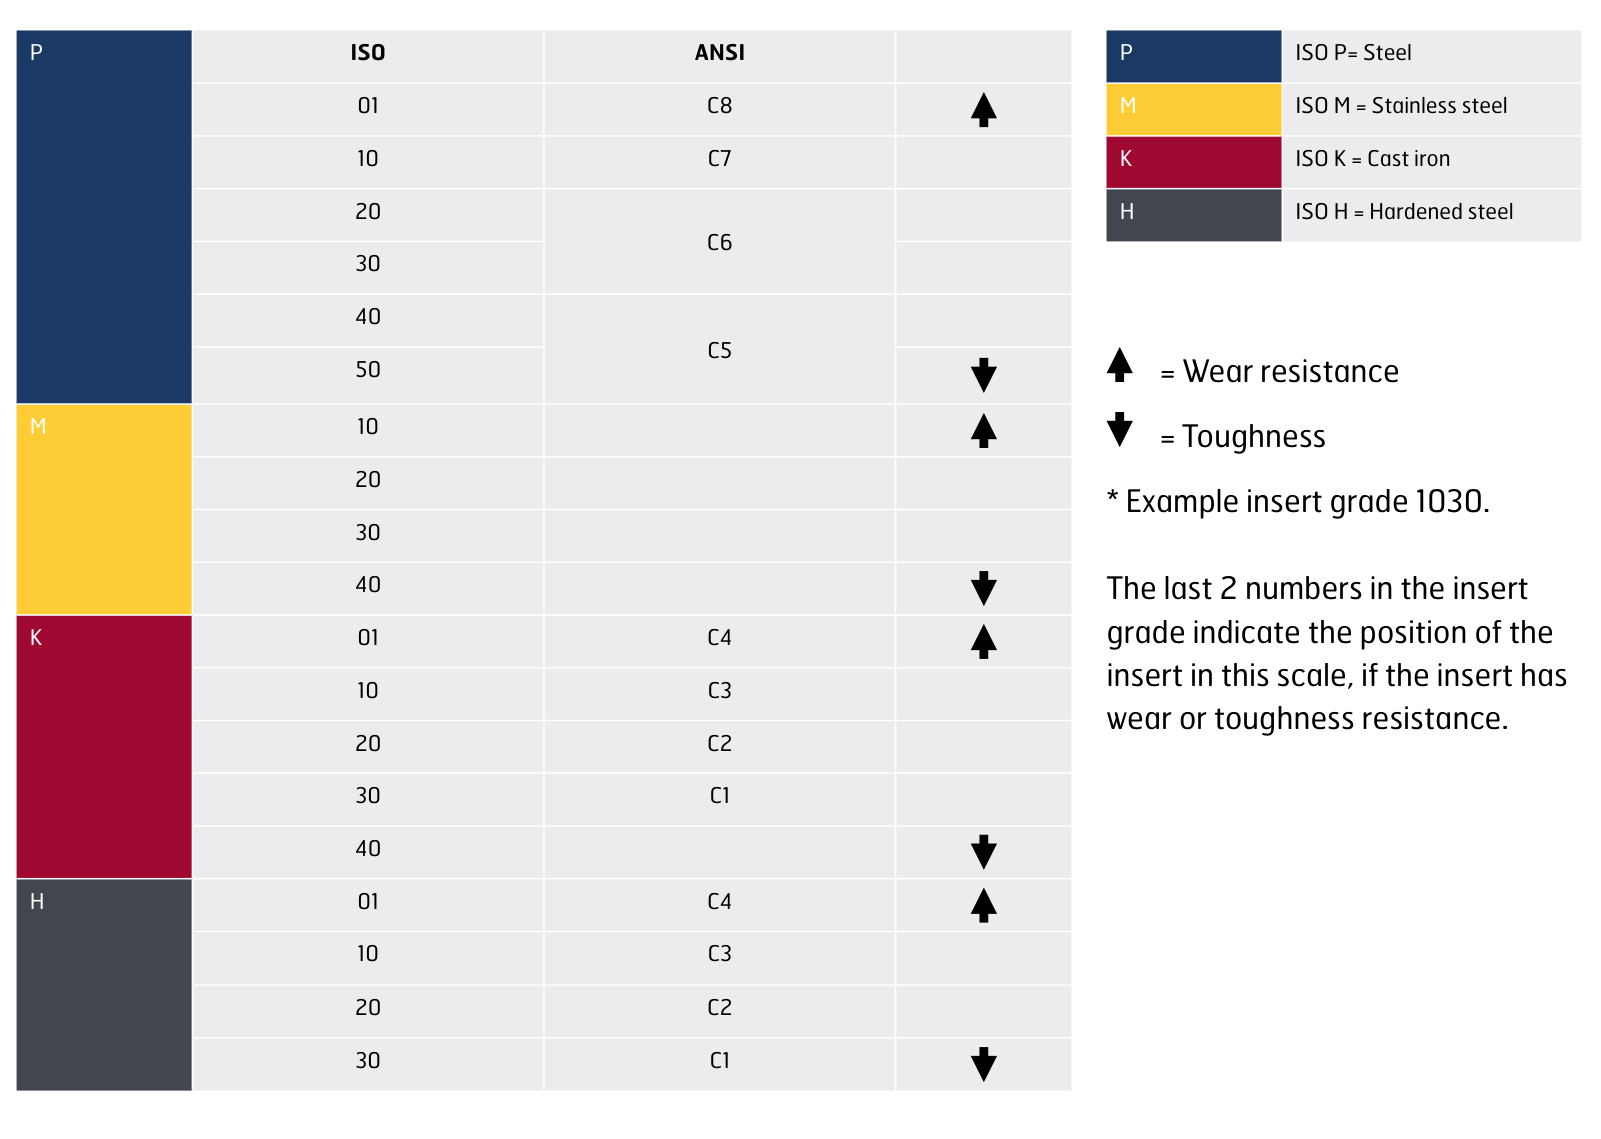
Insert grades for milling. ISO and ANSI grade codes against the P, M, K and H workpiece material classes, with the wear-resistance and toughness direction of the scale. The last two numbers in the insert grade indicate the position of the insert in this scale — example insert grade 1030.
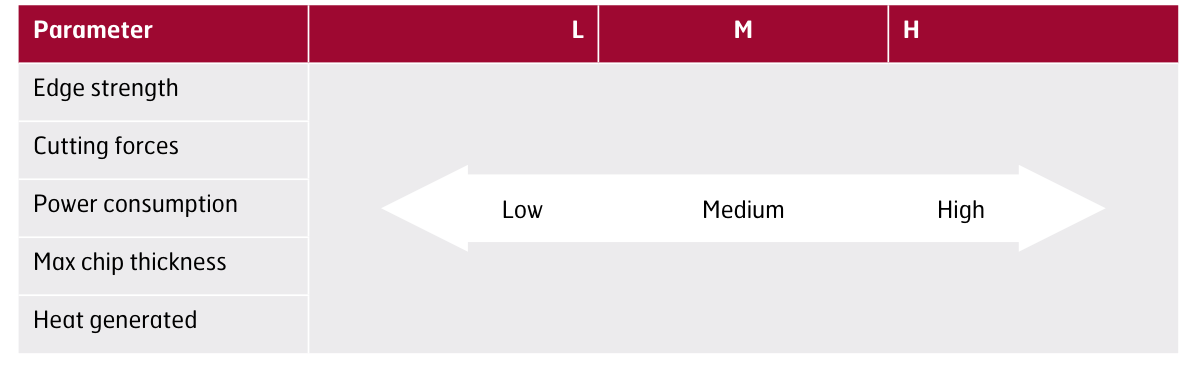
Insert geometry. Edge strength, cutting forces, power consumption, maximum chip thickness and heat generated across the L, M and H geometries.
Face milling recommendation with a 45° setting angle
Face milling, 45° setting angle. Cutting speed and feed per tooth by grade. Columns give feed per tooth, (fz) mm/t.
Steel grade | Cutting speed (Vc), m/min | min — Insert grade P30 | max — Insert grade P30 |
|---|---|---|---|
Hardox® HiTemp | 120 – 160 | 0.10 | 0.25 |
Hardox® HiAce | 100 – 140 | * 0.10 | * 0.25 |
Hardox® HiTuf | 140 – 180 | 0.10 | 0.25 |
Hardox® 400 | 120 – 160 | 0.10 | 0.25 |
Hardox® 450 | 110 – 150 | 0.10 | 0.25 |
Hardox® 500 | 100 – 140 | 0.10 | 0.25 |
Hardox® 500 Tuf | 100 – 140 | 0.10 | 0.25 |
Hardox® 550 | 70 – 90 | 0.10 | 0.20 |
Hardox® 600 | 50 – 70 | 0.10 | 0.20 |
Hardox® Extreme | 30 – 50 | 0.10 | 0.20 |
Face milling recommendation with round inserts
Face milling with round inserts. Cutting speed and feed per tooth by grade. Columns give feed per tooth, (fz) mm/t.
Steel grade | Cutting speed (Vc), m/min | min — Insert grade P30 | max — Insert grade P30 |
|---|---|---|---|
Hardox® HiTemp | 120 – 160 | 0.10 | 0.25 |
Hardox® HiAce | 100 – 140 | * 0.10 | * 0.25 |
Hardox® HiTuf | 140 – 180 | 0.10 | 0.25 |
Hardox® 400 | 120 – 160 | 0.10 | 0.25 |
Hardox® 450 | 110 – 150 | 0.10 | 0.25 |
Hardox® 500 | 100 – 140 | 0.10 | 0.25 |
Hardox® 500 Tuf | 100 – 140 | 0.10 | 0.25 |
Hardox® 550 | 70 – 90 | 0.10 | 0.25 |
Hardox® 600 | 50 – 70 | 0.10 | 0.20 |
Hardox® Extreme | 30 – 50 | 0.10 | 0.20 |
Shoulder milling recommendation with a 90° setting angle
Shoulder milling, 90° setting angle. Cutting speed and feed per tooth by grade. Columns give feed per tooth, (fz) mm/t.
Steel grade | Cutting speed (Vc), m/min | min — Insert grade P30 | max — Insert grade P30 |
|---|---|---|---|
Hardox® HiTemp | 120 – 160 | 0.12 | 0.25 |
Hardox® HiAce | 100 – 140 | * 0.12 | * 0.25 |
Hardox® HiTuf | 140 – 180 | 0.12 | 0.25 |
Hardox® 400 | 120 – 160 | 0.12 | 0.25 |
Hardox® 450 | 110 – 150 | 0.12 | 0.25 |
Hardox® 500 | 100 – 140 | 0.12 | 0.25 |
Hardox® 500 Tuf | 100 – 140 | 0.12 | 0.25 |
Hardox® 550 | 70 – 90 | 0.10 | 0.20 |
Hardox® 600 | 50 – 70 | 0.10 | 0.20 |
Hardox® Extreme | 30 – 50 | 0.10 | 0.20 |
High feed milling with CoroMill 210, 10° setting angle
High feed milling, CoroMill 210. Cutting speed and feed per tooth by grade and insert size. Columns give feed per tooth, (fz) mm/t.
Steel grade | Cutting speed (Vc), m/min | Min Insert grade P30 — Insert size 09 | Max Insert grade P30 — Insert size 09 | Min Insert grade P30 — Insert size 14 | Max Insert grade P30 — Insert size 14 |
|---|---|---|---|---|---|
Hardox® HiTemp | 120 – 160 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® HiAce | 90 – 130 | * 0.4 | * 2.0 | * 0.5 | * 3.0 |
Hardox® HiTuf | 140 – 180 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 400 | 120 – 160 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 450 | 110 – 150 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 500 | 90 – 130 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 500 Tuf | 90 – 130 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 550 | 70 – 90 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® 600 | 50 – 70 | 0.4 | 2.0 | 0.5 | 3.0 |
Hardox® Extreme | 35 – 50 | 0.4 | 2.0 | 0.5 | 3.0 |
Hole making with high feed milling (circular ramping)
Circular ramping with a high feed cutter is an alternative to drilling for larger holes. Use the cutting data for high feed milling above.
Shoulder milling recommendation
Shoulder milling. Cutting speed and feed per tooth by cutter diameter. Columns give feed per tooth, (fz) mm/t / Min – Max.
Steel grade | Cutting speed (Vc), m/min | Ø Diameter 3.0 – 6.0 | Ø Diameter 8.0 – 12.0 | Ø Diameter 14.0 – 20.0 |
|---|---|---|---|---|
Hardox® HiTemp | 75 – 100 | 0.01 – 0.03 | 0.03 – 0.06 | 0.06 – 0.09 |
Hardox® HiAce | 65 – 90 | 0.01 – 0.03 | 0.03 – 0.05 | 0.05 – 0.07 |
Hardox® HiTuf | 80 – 105 | 0.01 – 0.03 | 0.04 – 0.07 | 0.07 – 0.10 |
Hardox® 400 | 75 – 100 | 0.01 – 0.03 | 0.03 – 0.06 | 0.06 – 0.09 |
Hardox® 450 | 70 – 95 | 0.01 – 0.03 | 0.03 – 0.06 | 0.06 – 0.08 |
Hardox® 500 | 45 – 70 | 0.01 – 0.025 | 0.03 – 0.05 | 0.05 – 0.07 |
Hardox® 500 Tuf | 45 – 70 | 0.01 – 0.025 | 0.03 – 0.05 | 0.05 – 0.07 |
Hardox® 550 | 40 – 65 | 0.01 – 0.02 | 0.03 – 0.045 | 0.05 – 0.065 |
Hardox® 600 | 30 – 40 | 0.005 – 0.015 | 0.02 – 0.03 | 0.03 – 0.04 |
Hardox® Extreme | 20 – 30 | 0.005 – 0.01 | 0.015 – 0.025 | 0.025 – 0.035 |
End milling recommendation for solid cemented carbide tool
End milling, solid cemented carbide. Cutting speed and feed per tooth by cutter diameter. Columns give feed per tooth, (fz) mm/t / Min – Max.
Steel grade | Cutting speed (Vc), m/min | Ø Diameter 3.0 – 6.0 | Ø Diameter 8.0 – 12.0 | Ø Diameter 14.0 – 20.0 |
|---|---|---|---|---|
Hardox® HiTemp | 180 – 210 | 0.02 – 0.04 | 0.06 – 0.09 | 0.10 – 0.13 |
Hardox® HiAce | 120 – 150 | 0.015 – 0.35 | 0.05 – 0.07 | 0.08 – 0.10 |
Hardox® HiTuf | 190 – 220 | 0.02 – 0.05 | 0.06 – 0.10 | 0.10 – 0.13 |
Hardox® 400 | 180 – 210 | 0.02 – 0.04 | 0.06 – 0.09 | 0.10 – 0.13 |
Hardox® 450 | 160 – 190 | 0.02 – 0.04 | 0.06 – 0.09 | 0.10 – 0.12 |
Hardox® 500 | 120 – 150 | 0.015 – 0.35 | 0.05 – 0.07 | 0.08 – 0.10 |
Hardox® 500 Tuf | 120 – 150 | 0.015 – 0.35 | 0.05 – 0.07 | 0.08 – 0.10 |
Hardox® 550 | 80 – 110 | 0.01 – 0.035 | 0.045 – 0.07 | 0.08 – 0.10 |
Hardox® 600 | 70 – 100 | 0.01 – 0.035 | 0.04 – 0.07 | 0.08 – 0.10 |
Hardox® Extreme | 60 – 90 | 0.01 – 0.03 | 0.04 – 0.06 | 0.06 – 0.08 |
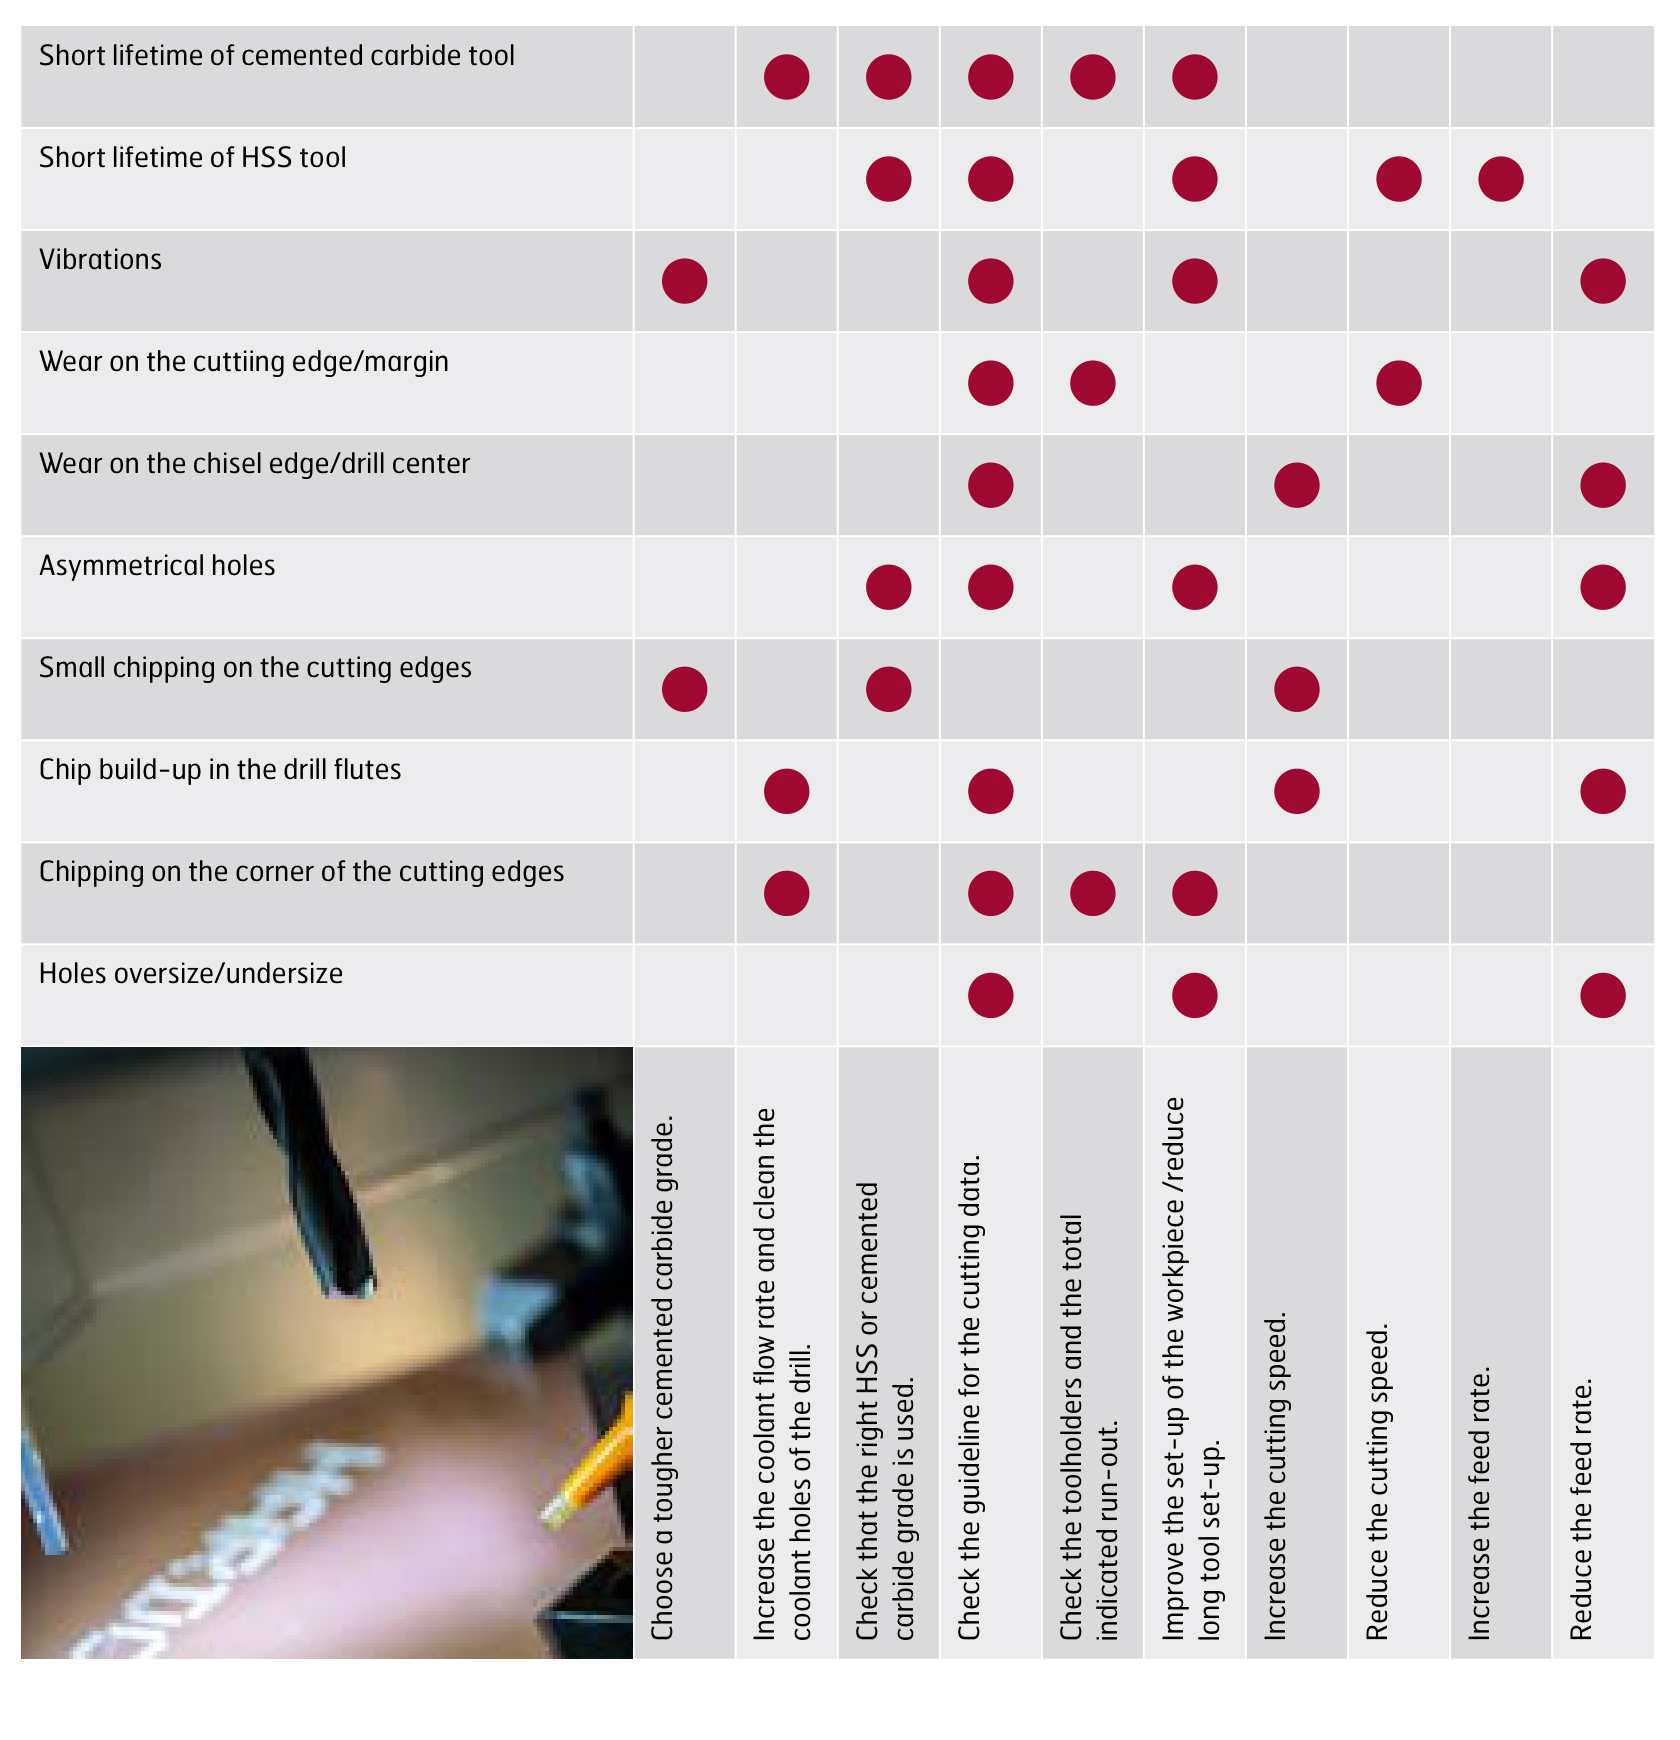
Troubleshooting for drilling
Symptom against cause. A dot marks a remedy that applies to that symptom.
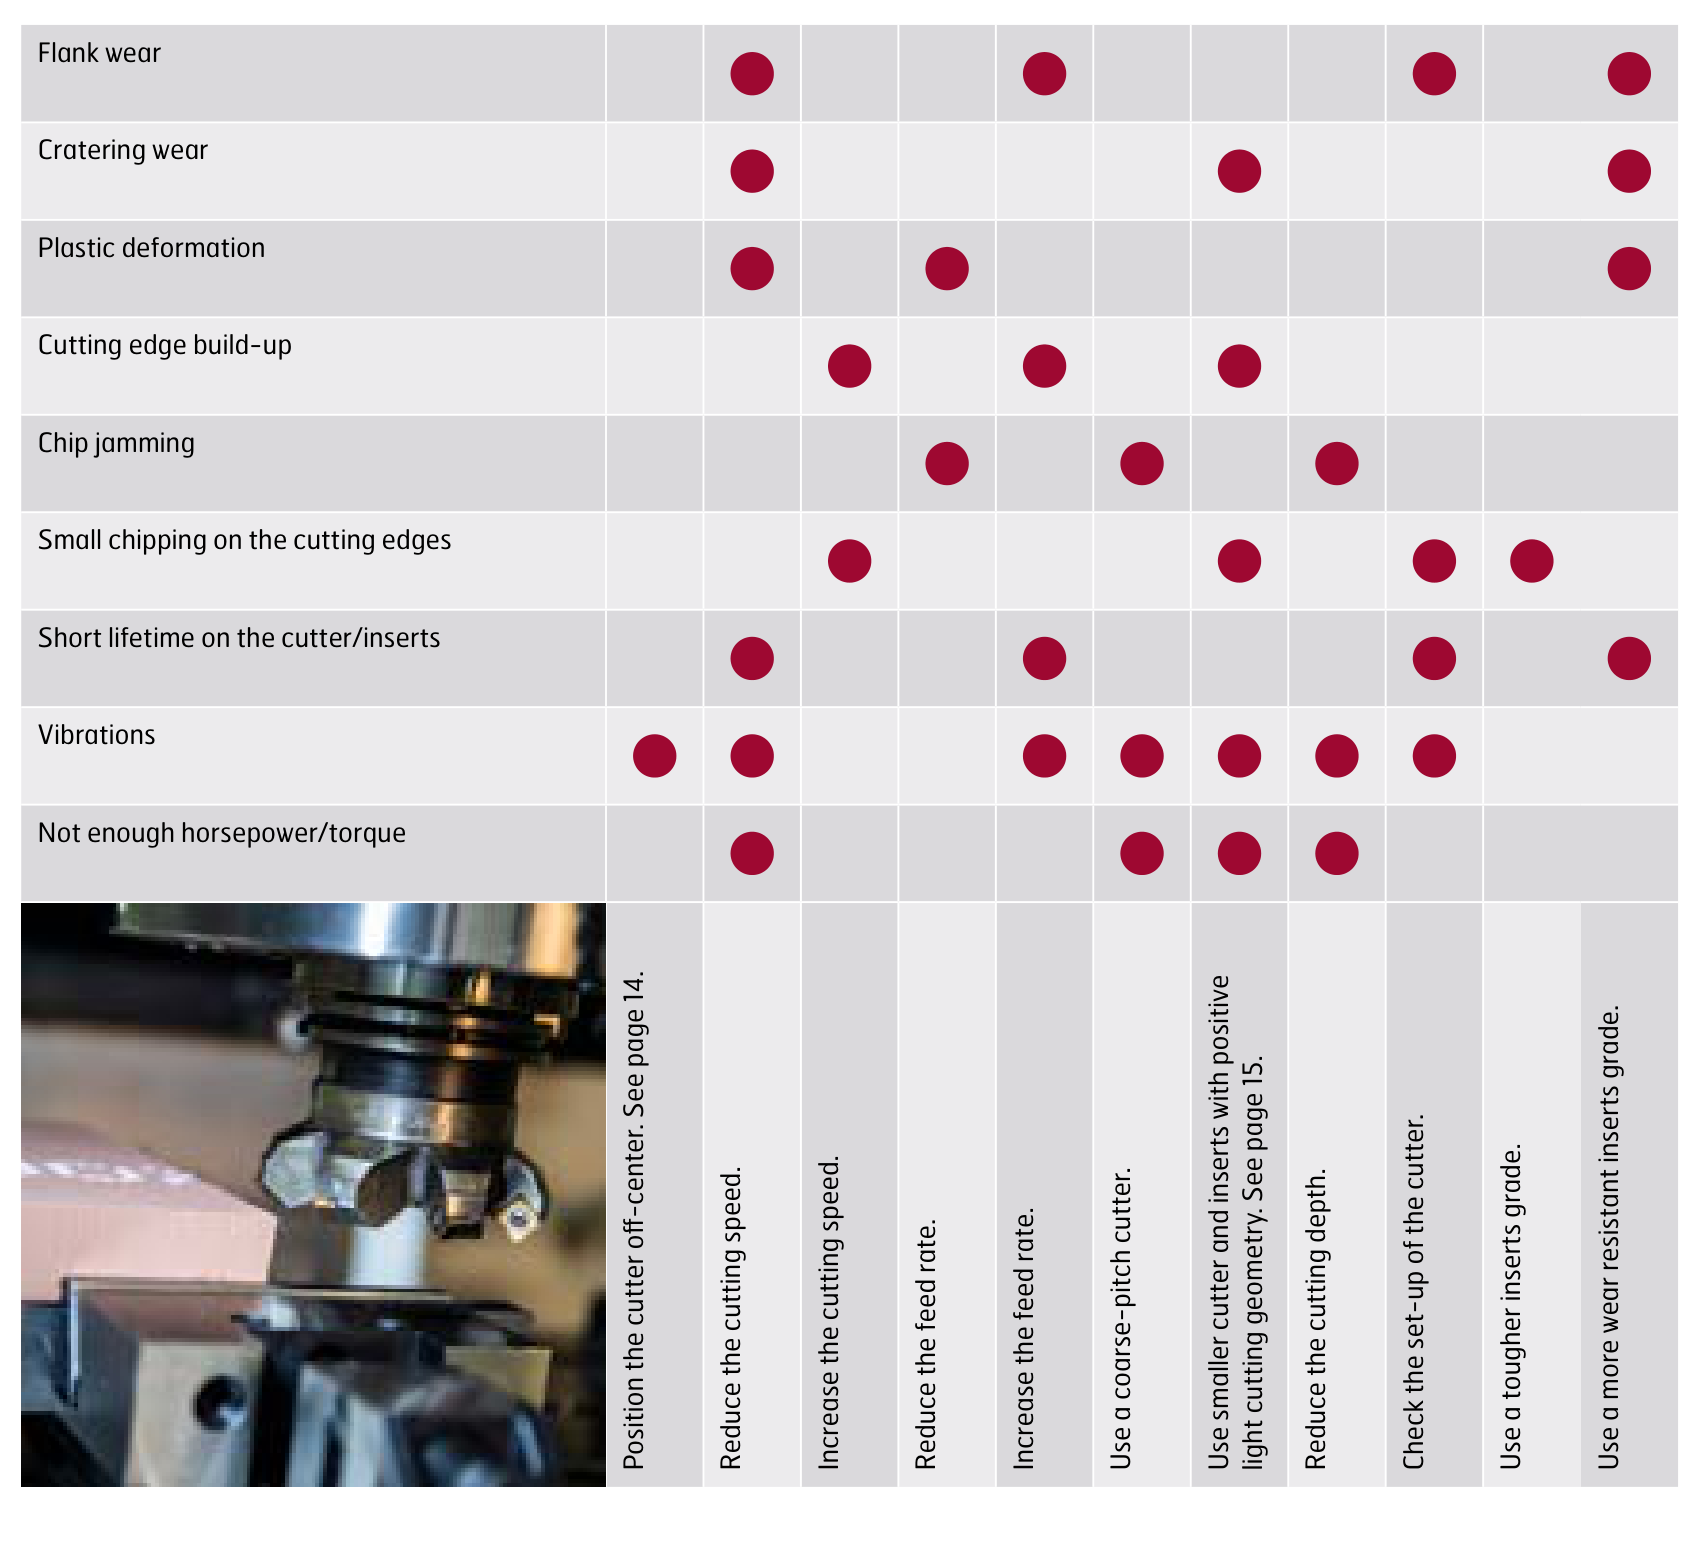
Troubleshooting for milling
Symptom against cause. A dot marks a remedy that applies to that symptom.
Turning recommendations
The cutting data recommendations below are applicable for tough cemented carbide grades. These grades are necessary for operations in which impact may occur, such as when turning plate with gas-cut edges. At higher feed rate, reduce the cutting speed.
Formulas and definitions, turning
- Vc = Dm × π × n / 1000
- n = Vc × 1000 / (π × Dm)
- vf = n × fn
- π = 3.142
- Vc = cutting speed (m/min)
- n = spindle speed (rpm)
- fn = feed per revolution (mm/rev)
- vf = feed rate (mm/min)
- Dm = machined diameter (mm)
- ap = cutting depth (mm)
Turning. Cutting speed by insert grade. The three speeds in each cell correspond to the three feed rates for that insert grade: 0.1 – 0.4 – 0.8 mm/rev for P25 and P35, and 0.1 – 0.3 mm/rev for K20.
Steel grade | Insert grade P25 / C6 — Vc (m/min) | Insert grade P35 / C6-C7 — Vc (m/min) | Insert grade K20 / C2 — Vc (m/min) |
|---|---|---|---|
Hardox® HiTemp | 130 – 90 – 70 | 105 – 65 – 45 | |
Hardox® HiAce | 100 – 80 | ||
Hardox® HiTuf | 130 – 90 – 70 | 105 – 65 – 45 | |
Hardox® 400 | 130 – 90 – 70 | 105 – 65 – 45 | |
Hardox® 450 | 130 – 90 – 70 | 105 – 65 – 45 | |
Hardox® 500 | – | 100 – 80 | |
Hardox® 500 Tuf | – | 100 – 80 |
Results from our own tests
The tables below record the machines and cutting data used in SSAB’s own tests.
Test. * Hardox® 500.
* Hardox® 500 | Tool | drill Ø | Ø | Vc | Thread depth | Total |
|---|---|---|---|---|---|---|
Tapping/through holes | Manigley 105/4 DUO | 21.5 | M24 | 3.4 | 40 mm | 48 |
Test. * Hardox® 500.
* Hardox® 500 | Tool | Ø | Vc | fn | Drill depth | Total |
|---|---|---|---|---|---|---|
Drilling/through holes | HSS Co 5% X-Alcr | 18 | 5 | 0.17 | 30 mm | 33 |
Test. Hardox® 500.
Hardox® 500 | Tool | Ø | Vc | fn | Drill depth | Total |
|---|---|---|---|---|---|---|
Drilling/through holes | EF dril | 10.4 | 40 | 0.1 | 30 mm | 875 |
Test. Hardox® 500.
Hardox® 500 | Tool | drill Ø | Ø | Vc | Thread depth | Total |
|---|---|---|---|---|---|---|
Tapping/through holes | Manigley 105/4 DUO | 10.4 | M12 | 3 | 30 mm | 161 |
Test. Hardox® 600.
Hardox® 600 | Tool | Ø | Vc | fn | Drill depth | Total |
|---|---|---|---|---|---|---|
Drilling/through holes | ChamDrill | 18 | 30 | 0.1 | 30 mm | 180 |
Test. Hardox® Extreme.
Hardox® Extreme | Tool | Ø | Vc | fn | Drill depth | Total |
|---|---|---|---|---|---|---|
Drilling/through holes | MPS1 (DP 1021) | 12 | 25 | 0.1 | 25 mm | 403 |
Tool recommendations for Hardox® wear plate
The tools below are grouped by type. Article numbers are reproduced exactly as SSAB prints them, including the wildcard characters that stand for the size-dependent part of the number.
High speed steel drill. High speed steel drill alloyed with 8% cobalt (HSS-Co 8%), or alloyed with cobalt.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
MayKestag, Austria | HSS-E Co 8 Taper Shank Drills, WN 103 | 832xxxxx | https://www.maykestag.com/en/ |
Witec, Germany | TYPE WITEC MN | 2-135 15 VAP | http://www.witec-tools.de/ |
Somta, South Africa | MTS Armour Piercing drill | 261xxxx | https://www.somta.co.za/ |
Izar, Spain | Ref 1054 | 32xxx | https://www.izartool.com/ |
Izar, Spain | Ref 1154 | xxxxx | https://www.izartool.com/ |
Presto tools, England | Armour Piercing drill (APX) | 11211xx.xx | https://www.presto-tools.co.uk/ |
Solid cemented carbide drill. Solid cemented carbide drill.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Emuge Franken, Germany | EF-Drill-STEEL | TA203344xx.xx | https://www.emuge-franken-group.com |
Sandvik Coromant AB, Sweden | Corodrill R840 Delta C | R840-xxxx-30-A1A | https://www.sandvik.coromant.com/ |
Granlund Tool AB, Sweden | Tunder / T80 | T80-xx.x | http://www.granlund.com/ |
Mitsubishi, Japan | MPS1 (DP 1021) | MPS1-xxxxS | http://www.mitsubishicarbide.com/ |
Seco, Sweden | Seco Feedmax | SD203A-xx.x-xx-xxxx-M | https://www.secotools.com/ |
WNT, Germany | WTX-UNI | 11780 | https://cuttingtools.ceratizit.com/gb/en.html |
Hoffman-Group, Germany | Garant 122500 | 122500 | https://www.hoffmann-group.com/ |
Drill with exchangeable drill tip. Drill with exchangeable drill tip.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Iscar, Israel | Chamdrill | DCM xxx-xxx-xxA-3D | https://www.iscar.com |
Iscar, Israel | SumoCham | DCN xxx-xxx-xxA-3D | https://www.iscar.com |
Hoffman-Group, Germany | HiPer-Drill | 23 1605 -xx.x | https://www.hoffmann-group.com/ |
Sandvik Coromant, Sweden | CoroDrill 870 | 870-xxxx-xxxx | https://www.sandvik.coromant.com |
Indexable insert drill. Indexable insert drill.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Sandvik Coromant, Sweden | CoroDrill 880 | 880-Dxxxxxxx-xx | https://www.sandvik.coromant.com |
Counterbore and countersink. Counterbore and countersink tools.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Granlund Tool AB, Sweden | WHV counterbore | xWHV-xx.x | http://www.granlund.com/ |
Granlund Tool AB, Sweden | KV countersink | xKV9-xx.x | http://www.granlund.com/ |
Taps. Taps for through holes and blind holes.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Manigley, Switzerland | 105/4 DUO | 433xx | http://www.manigley.ch/de/home |
Manigley, Switzerland | 131/3 DUO | 433xx | http://www.manigley.ch/de/home |
Sandvik Coromant, Sweden | CoroTap 200 | E324 / E326 | https://www.sandvik.coromant.com/ |
Hoffman-Group, Germany | Garant 132065 | 132065-Mxx | https://www.hoffmann-group.com/ |
BASS, Germany | VARIANT 1/2 TIH | 1088xx | https://www.bass-tools.com/ |
Thread mills. Solid carbide thread mills.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Emuge Franken, Germany | GF-VZ-VHM-R15-IKZ-HB | GFB35106.xxxx | https://www.emuge.de/ |
Emuge Franken, Germany | GSF-VHM 2D IKZ-HB | GF333106.xxxx | https://www.emuge.de/ |
End mills. Solid carbide end mills.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Seco Tool, Sweden | JS 554 Siron-A | JS554xxxx | https://www.secotools.com/ |
Milling with inserts. Face milling, shoulder milling and high-feed holemaking with indexable inserts.
Supplier | Tool name | Article nr | Web |
|---|---|---|---|
Sandvik Coromant, Sweden | Coromill 345 | 345-xxxxxx-13x | https://www.sandvik.coromant.com/ |
Sandvik Coromant, Sweden | Coromill 300 | R300-xxxxxx-xxx | https://www.sandvik.coromant.com/ |
Sandvik Coromant, Sweden | Coromill 490 | 490-xxxxxx-xxx | https://www.sandvik.coromant.com/ |
Sandvik Coromant, Sweden | Coromill 210 | R210-xxxxxx-xxx | https://www.sandvik.coromant.com/ |
Insert grade in Hardox® steel. CoroMill article numbers and insert geometry.
Tool name | Article nr/insert grade | Insert geometry |
|---|---|---|
Coromill 210 | R210-xxxxxx-Px / xx10 | M |
R210-xxxxxx-Px / xx30 | M | |
Coromill 300 | R300-xxxxxx-Px / xx10 | L-M-H |
R300-xxxxxx-Px / xx30 | L-M-H | |
Coromill 345 | 345R-xxxxxx-Px / xx10 | L-M-H |
345R-xxxxxx-Px / xx30 | L-M-H | |
Coromill 490 | 490R-xxxxxx-Px / xx10 | L-M |
490R-xxxxxx-Px / xx30 | L-M-H |
Tool suppliers we recommend and have collaborated with. Supplier and web address.
Tool supplier | Web |
|---|---|
Emuge Franken | www.emuge-franken.de |
Granlund Tools | www.granlund.com |
Hoffmann Group | www.hoffmann-group.com |
IZAR Cutting Tools | www.izartool.com |
ISCAR | www.iscar.com |
Komet Group | www.kometgroup.com |
Manigley | www.manigley.ch |
Mitsubishi | www.mitsubishicarbide.com |
Sandvik Coromant | www.sandvik.coromant.com |
SECO TOOLS | www.secotools.com |
Witech | www.witec-tools.de |
WNT | www.wnt.com |
Contact and more information
Contact your local SSAB representative or Tech Support at [email protected], or visit www.hardox.com.
The information contained in this brochure is provided only as general information. It is the user’s responsibility to independently determine suitability of all products and applications, and to test and verify the same.