




Duroxite® Welding
WELDING
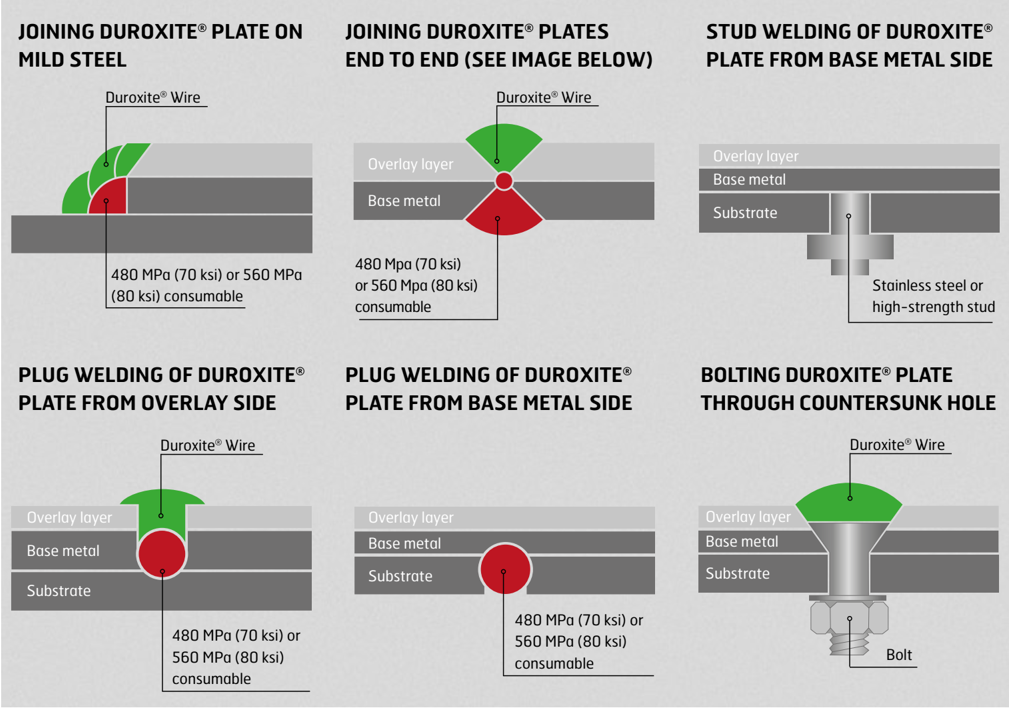
When joining plates of Duroxite®, start by joining the base metal with 480 MPa (70 ksi) or 560 MPa (80 ksi) consumables. Any surface exposed to severe wear should be protected with hardsurfacing consumables.
Cap welding a Duroxite® product with Duroxite® WIRE ensures the weld will have the same wear resistance, resulting in a consistent service life for the entire overlay product.
SAFETY PRECAUTIONS
When welding or cutting Duroxite® products, harmful fumes are produced that are chemically complex and difficult to classify. The major toxic component in the fumes is hexavalent chromium. Proper exhaust ventilation equipment and fume-extraction torches are recommended, as well as suitable protective clothing and respiratory protection for operators.
Duroxite® welding consumables come as both wire and electrodes for a variety of welding needs. They are used for production of overlay parts, maintenance and repair work.
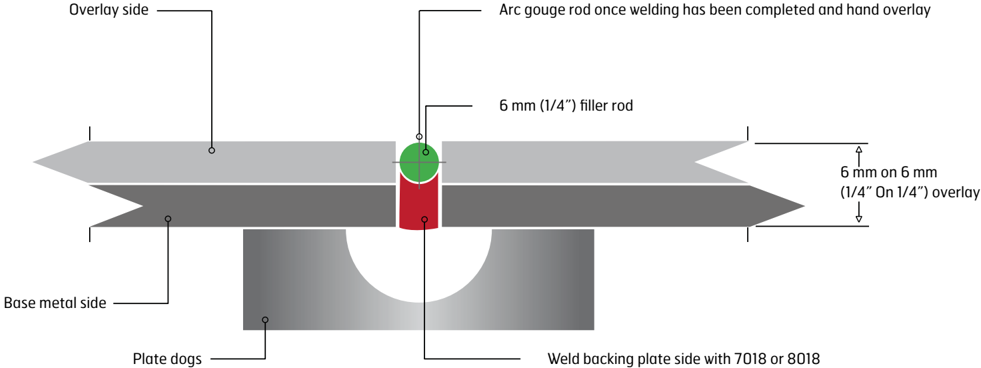
Joining two Duroxite® plates
Face overlay side down first. Insert a 6.4 mm (1/4”) filler rod and be sure to tack weld below backing plate. Install plate dogs to prevent plate distortion. Weld backing plate side, flip plate over, and arc gouge filler rod out. Fill gap flush with Duroxite® Wire. Turn plate back to backing plate side and remove plate dogs.